
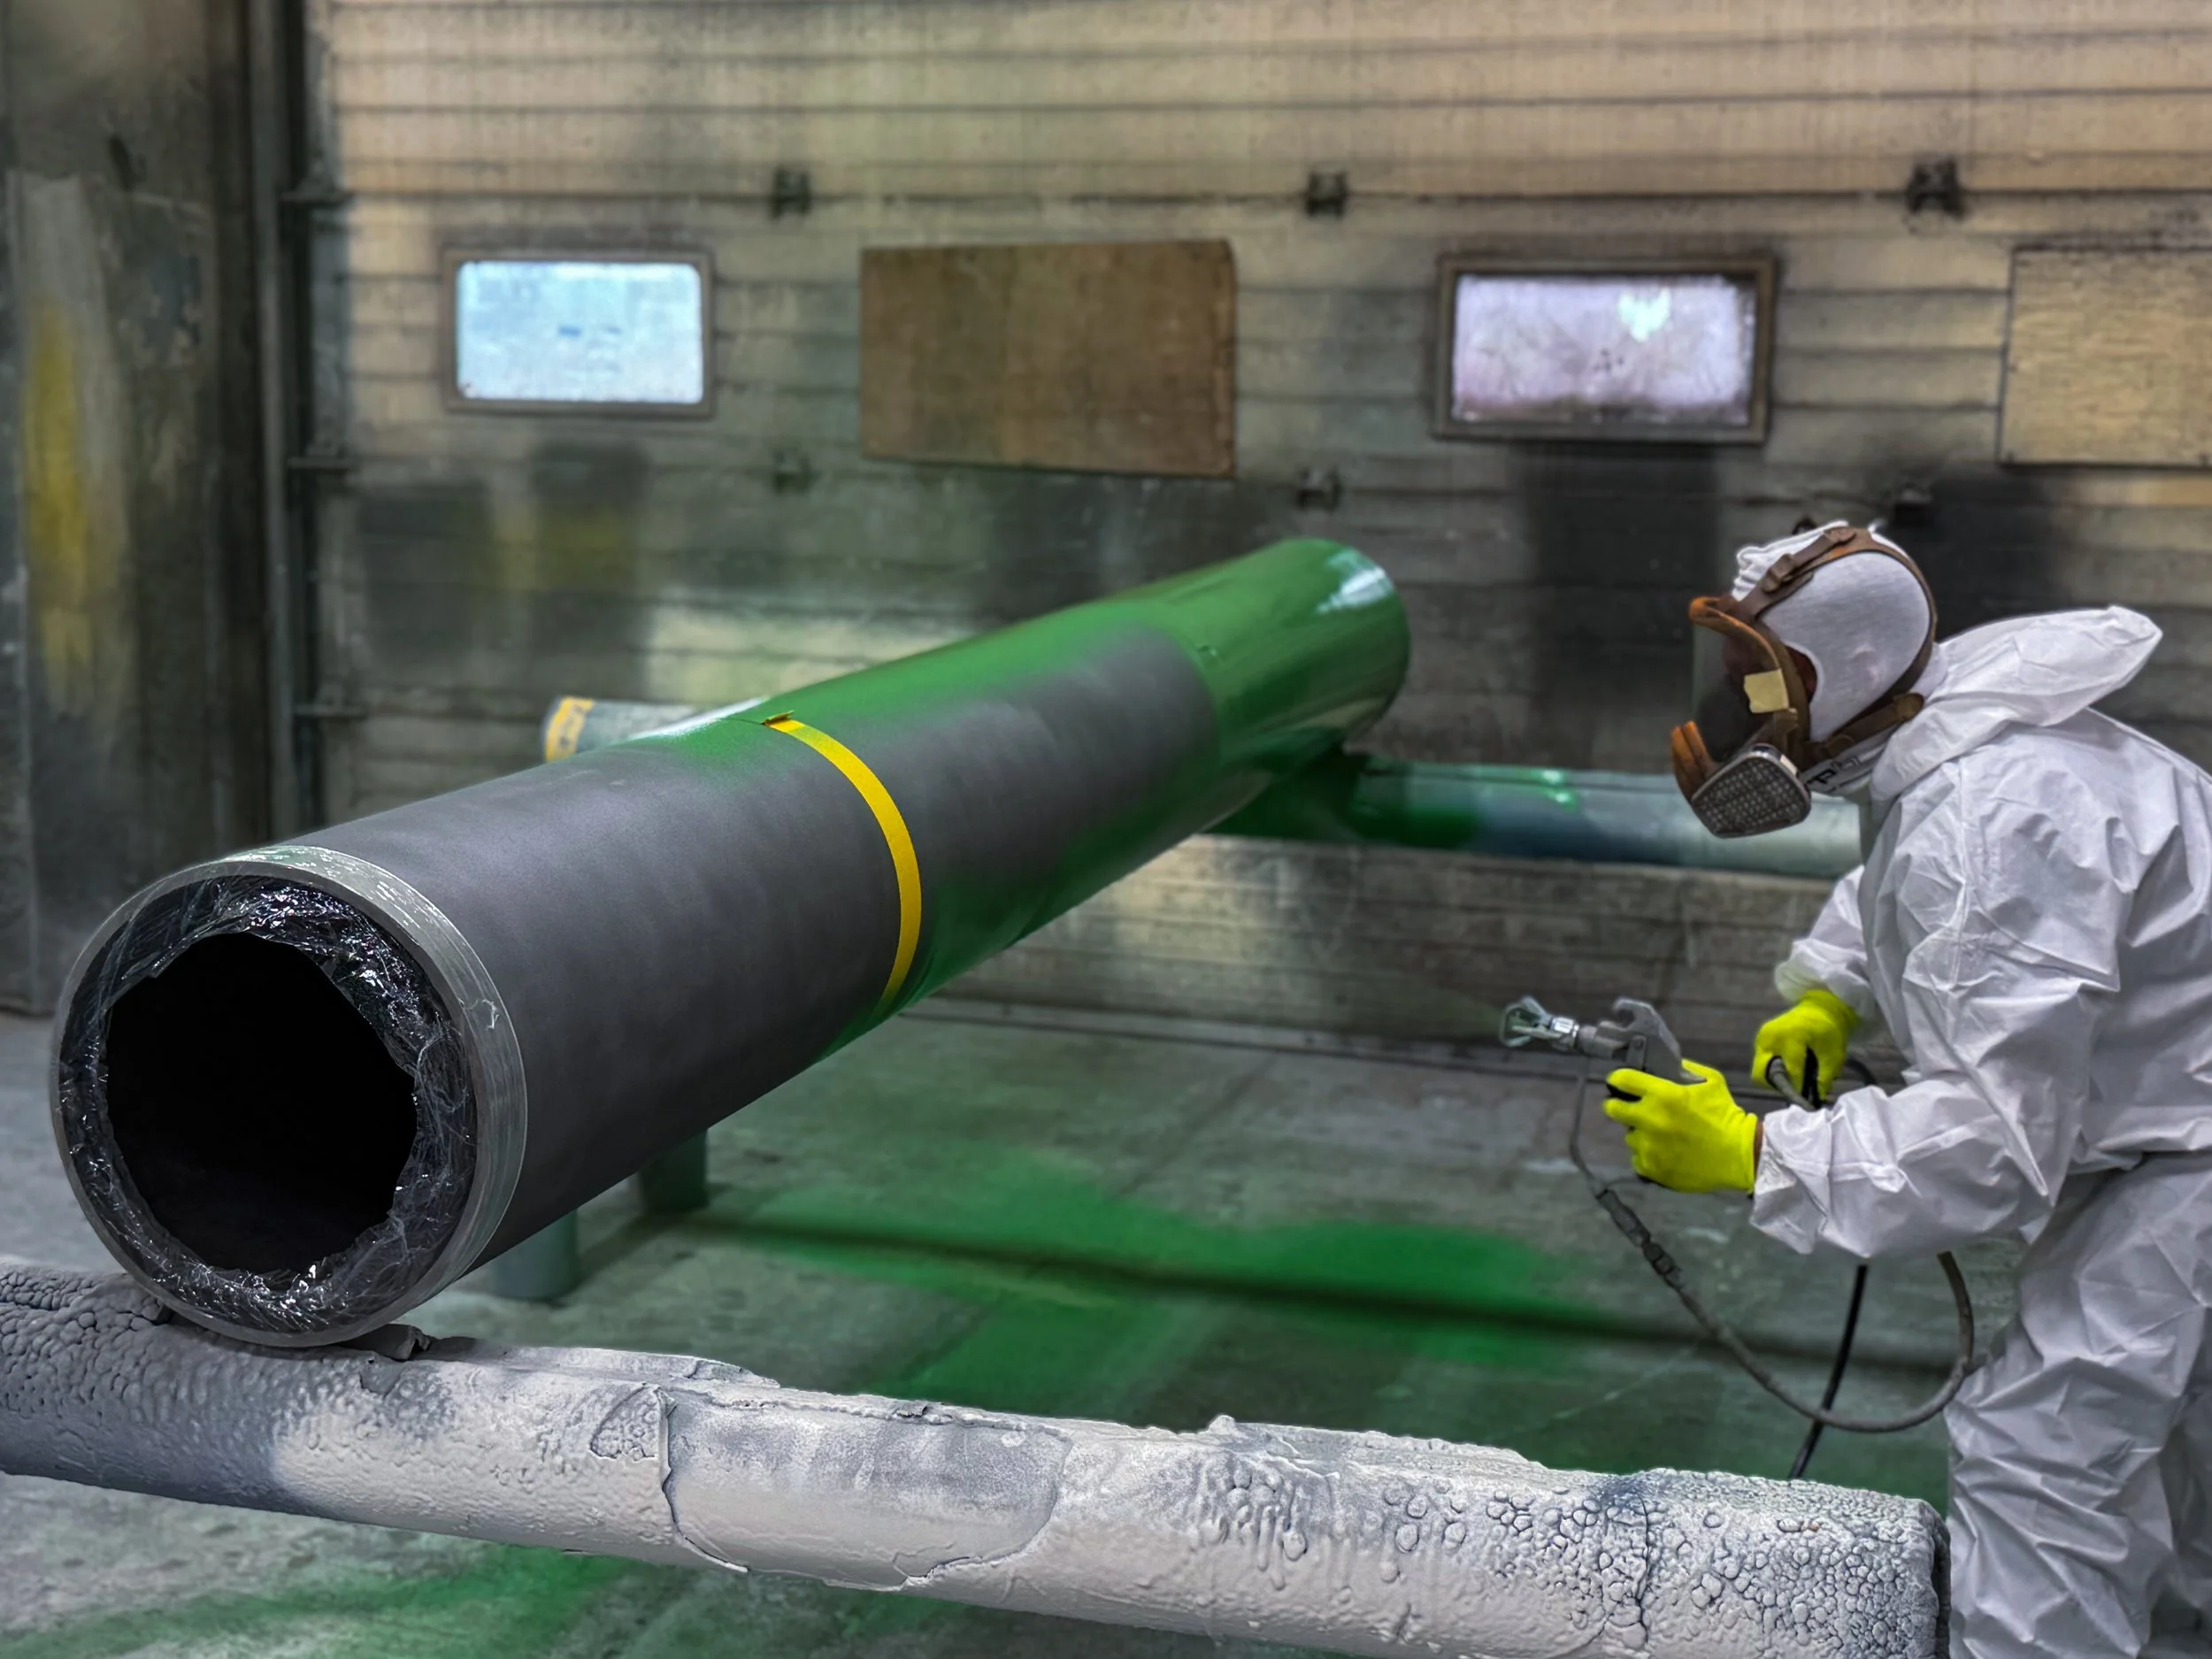
PIPELINE COATINGS ALBERTA
Custom Coatings International protects your pipelines, spools, and flow control components and extends their service life with coatings applied precisely to your specifications. Our NACE Level 2 & 3 certified inspectors perform the inspections and testing your specification requires, with full documentation to verify quality. Explore our Denso Protal 7200, Fusion Bonded Epoxy (FBE), and polyurethane coating systems below.
PIPELINE COATING OVERVIEW
What is the function of pipeline coatings?
Pipeline coatings serve as the first line of defense, primarily against internal and external corrosion, which degrades a pipeline’s structural integrity over time and can cause leaks and further damage to the pipeline and the surrounding environment.
Common pipeline coating systems and their applications
Pipeline coating refers to both internal and external specified pipeline coating systems. Common internal pipeline coatings include Fusion Bond Epoxy and liquid epoxies (such as Denso Protal 7200). External pipeline coating systems use one or two coats of Fusion Bond Epoxy, 3LPE & 3LPP systems, Liquid Epoxies, & Polyurethane coating systems.
The lifecycle cost benefits of pipeline coatings
Pipeline coating substantially extends the service life of pipeline assets, adding up to 15-25+ years of operational use. It is estimated that increasing the service life of pipeline assets by just 1% is enough to cover the cost of pipeline coatings, making it an easily justifiable investment to avoid production shutdowns, equipment & infrastructure damage, and protect the environment.
PIPELINE COATING OPTIONS
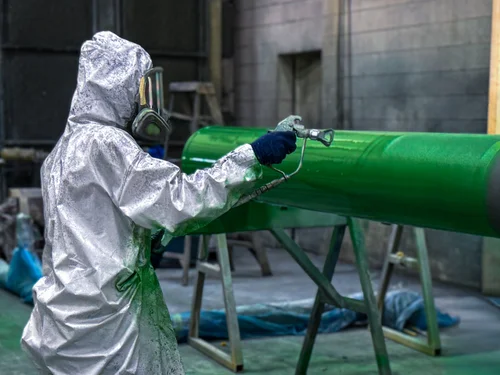
100% Solid Epoxies (Denso Protal 7200)
Denso Protal 7200 is the preferred external (and internal) coating for pipeline materials, corrosion, and integrity engineers because of its proven physical properties, adhesion performance, and reliable cure characteristics.
Key features
Fast touch-dry and set times
High temperature resistance up to 95°C (203°F)
High abrasion resistance and build (up to 70 mils / 1,778 µm per coat)
Strong chemical resistance
Meets sewage infrastructure AWWA C213 & C550, NSF/ANSI 61 specification standards
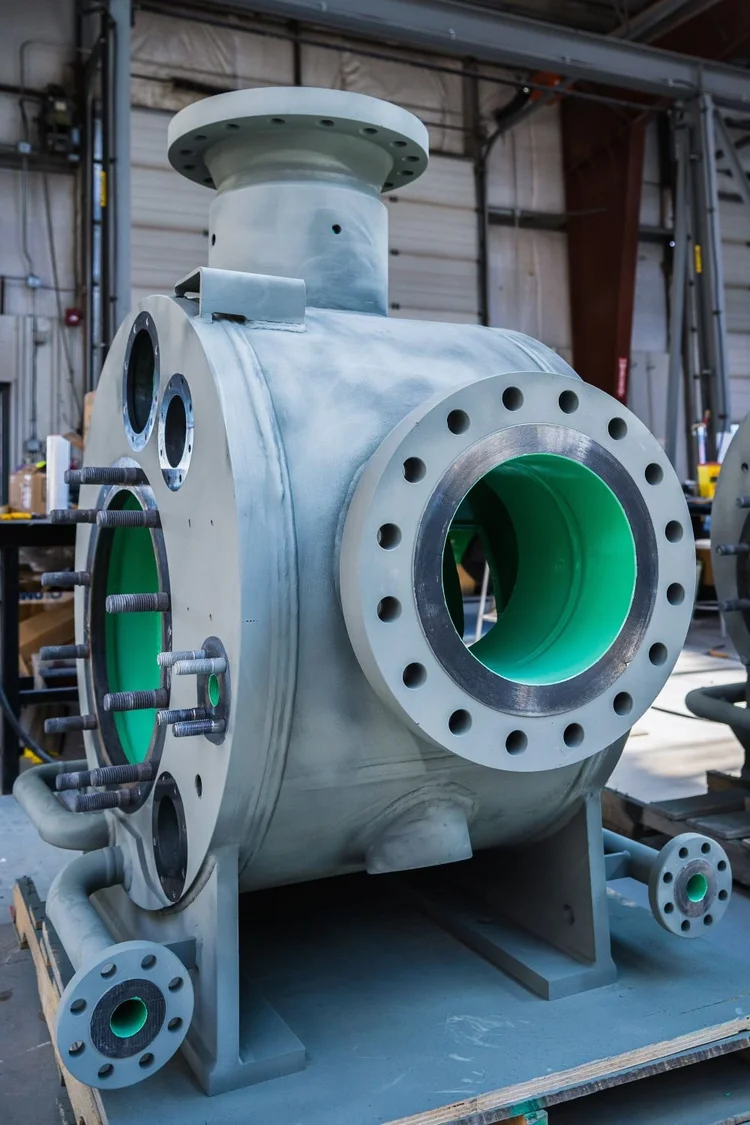
Fusion Bond Epoxy
FBE is a strong option for internal and external pipeline coatings. FBE is often specified because of its wide operating range, abrasion resistance, and superior chemical resistance.
Key features
Operational temperature of -100°F/-73°C to 203°F/95°C
Excellent anti-corrosive properties
The second layer can be specified for abrasion/impact resistance
High adhesion to steel substrate surface
Low disbondment
Follows CSA-Z245.20 Series-22
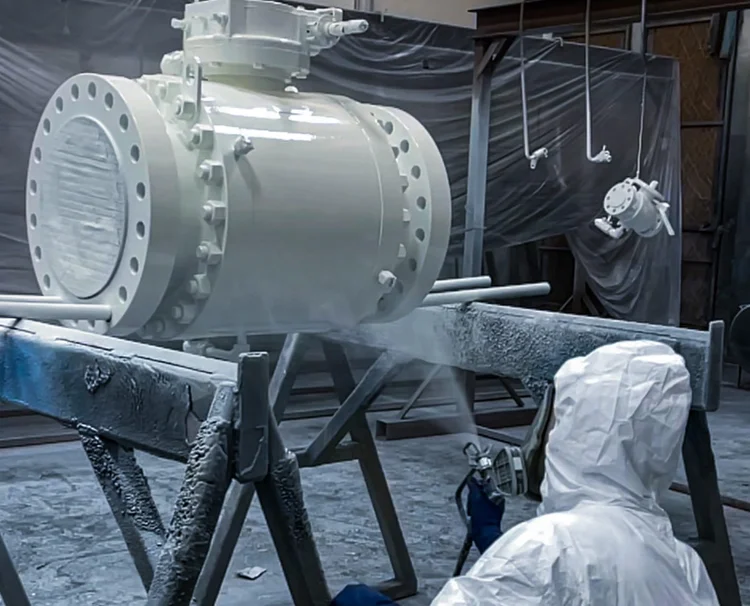
Polyurethane Coating
Polyurethane (including 100% solids, solventless, and elastomeric polyurethane) can be used as a primer or as a final coating. It is widely specified across oil/gas and water/wastewater pipeline, tank, and flow control component applications, and is easy to apply with no thermosetting required.
Key features
Strong chemical and corrosion resistance
Increased flexibility
High adhesion to metal substrate surfaces
Good impact and abrasion resistance
Strong UV stability (aliphatic polyurethanes)
THE IMPORTANCE OF PIPELINE COATING
According to the Alberta Energy Regulator, of the 277 pipeline incidents reported in 2025, 229 were pipeline failures. The two leading causes of pipeline failure include internal corrosion (38%) and external corrosion (13%). Additionally, 85% of licensed pipelines are made of steel, making them highly susceptible to corrosive damage.
Pipeline leaks & failures have many negative impacts, including environmental damage, repair and cleanup costs, and lost profits from operational downtime. Exact figures for annual pipeline failure costs in Canada are difficult to find, but it is theorized that costs exceed a few billion dollars annually. The investment in protective coating is clearly justified when a 1% increase in pipeline service life pays for the cost of pipeline coating.
Pipeline asset owners must invest in pipeline protection to prevent costly damage. This investment begins with developing a proper coating specification for your pipeline asset and finding a trusted coating applicator with years of experience adhering closely to specifications, accurately and on schedule. Custom Coatings International has 30+ years of industrial coating experience and NACE Level 1 & 2 inspectors on staff (with NACE Level 3 inspectors available upon request), with quality assurance supported by reviews from oil and gas industry leaders such as Baker Hughes and Halliburton - Summit ESP. Contact us for quotes and inquiries below:
INTERNAL & EXTERNAL PIPELINE COATINGS
Outside the pipe
External Coatings
External pipeline coatings serve as a protective barrier between the pipeline’s exterior steel surface and the external environment, whether it be soil, marine/immersed areas, or the outside environment. As with internal coatings, corrosion is the largest contributor to pipeline leaks and failures, especially under deposits and in microbiological, chemical (oxygen, hydrogen, hydrogen sulfide, etc.), atmospheric, & interference corrosion, which can occur under the coating or at valves or fittings.
Hover a card to highlight its layer
Inside the pipe
Internal Coatings
Internal pipeline coatings act as a barrier that protects the pipeline from the fluid. According to the Alberta Energy Regulator, the most common causes of internal corrosion include under-deposit corrosion, microbiologically influenced corrosion, interference, CO2 corrosion, and corrosion under internal coatings. Besides corrosion protection, internal pipeline coatings are designed to increase flow efficiency, prevent product contamination, and avoid internal deposition of fluid contaminants.

Credentials
- ISO 9001-certified, ISN member contractor, and COR-certified
- NACE Level 1 & 2 Certified Coating Inspectors on staff, with NACE Level 3 Certified Coating Inspectors available upon request
Quality Assurance & Control
- Surface preparation to SSPC/NACE standards, with profile measured and recorded per specification
- Climate-controlled blast and coating bays for proper application and cure
- QC testing, including ambient condition monitoring and DFT readings provided in every project
- X-cut adhesion, compressed air (blotter), dust, and soluble salt testing, and holiday testing available upon request
- Inspection and Test Plans (ITPs) and QC documentation available upon request
WHY CHOOSE CUSTOM COATINGS INTERNATIONAL?
CCI has invested significant resources in building and strengthening our quality assurance and control department, training our team to ensure every project meets specifications.
REQUEST A QUOTE
To initiate the quoting process, please provide the following information (if available):
• Drawings or isometrics
• Coating specifications
• Operating environment details (temperature range and chemical exposure)
• Project timeline or required completion date
We look forward to working with you on finding the right protective coating for your project. If you have any questions, please contact us using the links below.

Info@ccintl.ca for general inquiries

sales.support@ccintl.ca for quote requests