INDUSTRIAL COATINGS SERVICES IN ALBERTA
Industrial painting solutions designed to protect equipment from corrosion, wear, and extreme environments. Serving heavy industry within Alberta and Beyond with durable, high-performance coatings. Contact us to discuss your project and request a quote.
INDUSTRIAL COATINGS OVERVIEW
What are industrial coatings?
Industrial coatings refers to applying protective coating systems to industrial infrastructure (including pipes, spools, valves, tanks, and structural fabrications) to prevent corrosion, chemical attack, and mechanical degradation. Coating systems are specified by environment (atmospheric, buried, or immersed), corrosivity category (ISO 12944 C1–C5/Im), film build, and recoat requirements. Common systems include zinc-rich primers, epoxy intermediates, and polyurethane topcoats, selected based on service conditions and expected coating lifespan.
What types of industrial coatings does CCI apply?
CCI applies a range of industrial coating systems, including liquid-applied epoxies, high-build polyurethane topcoats, 100% solids epoxies (including Denso Protal 7200 for internal and external pipeline specifications), internal linings, coatings under insulation (CUI), and alkyd primer systems. For projects without an existing specification, CCI takes a consultative approach, assessing service conditions, environment, and substrate to recommend the coating system best suited to protect your components in the long term.
What are the main advantages of industrial coatings?
Correctly specified industrial coating systems can extend equipment service life by 15–25 years, significantly reducing lifecycle maintenance costs. Key protective functions include corrosion and chemical resistance (critical for pipelines and process vessels), abrasion and impact resistance for high-wear components, and thermal protection for equipment operating above 120°C. Beyond protection, coating systems reduce inspection frequency and unplanned downtime, two of the largest drivers of maintenance costs in industrial operations.
INDUSTRIAL COATINGS BY APPLICATION
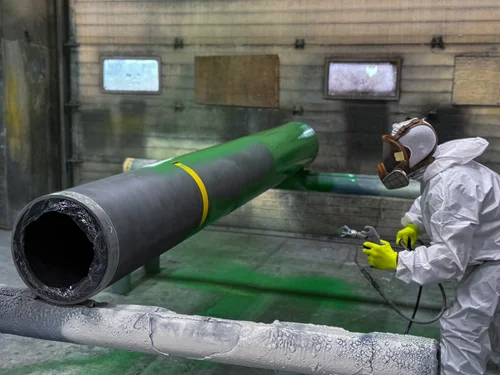
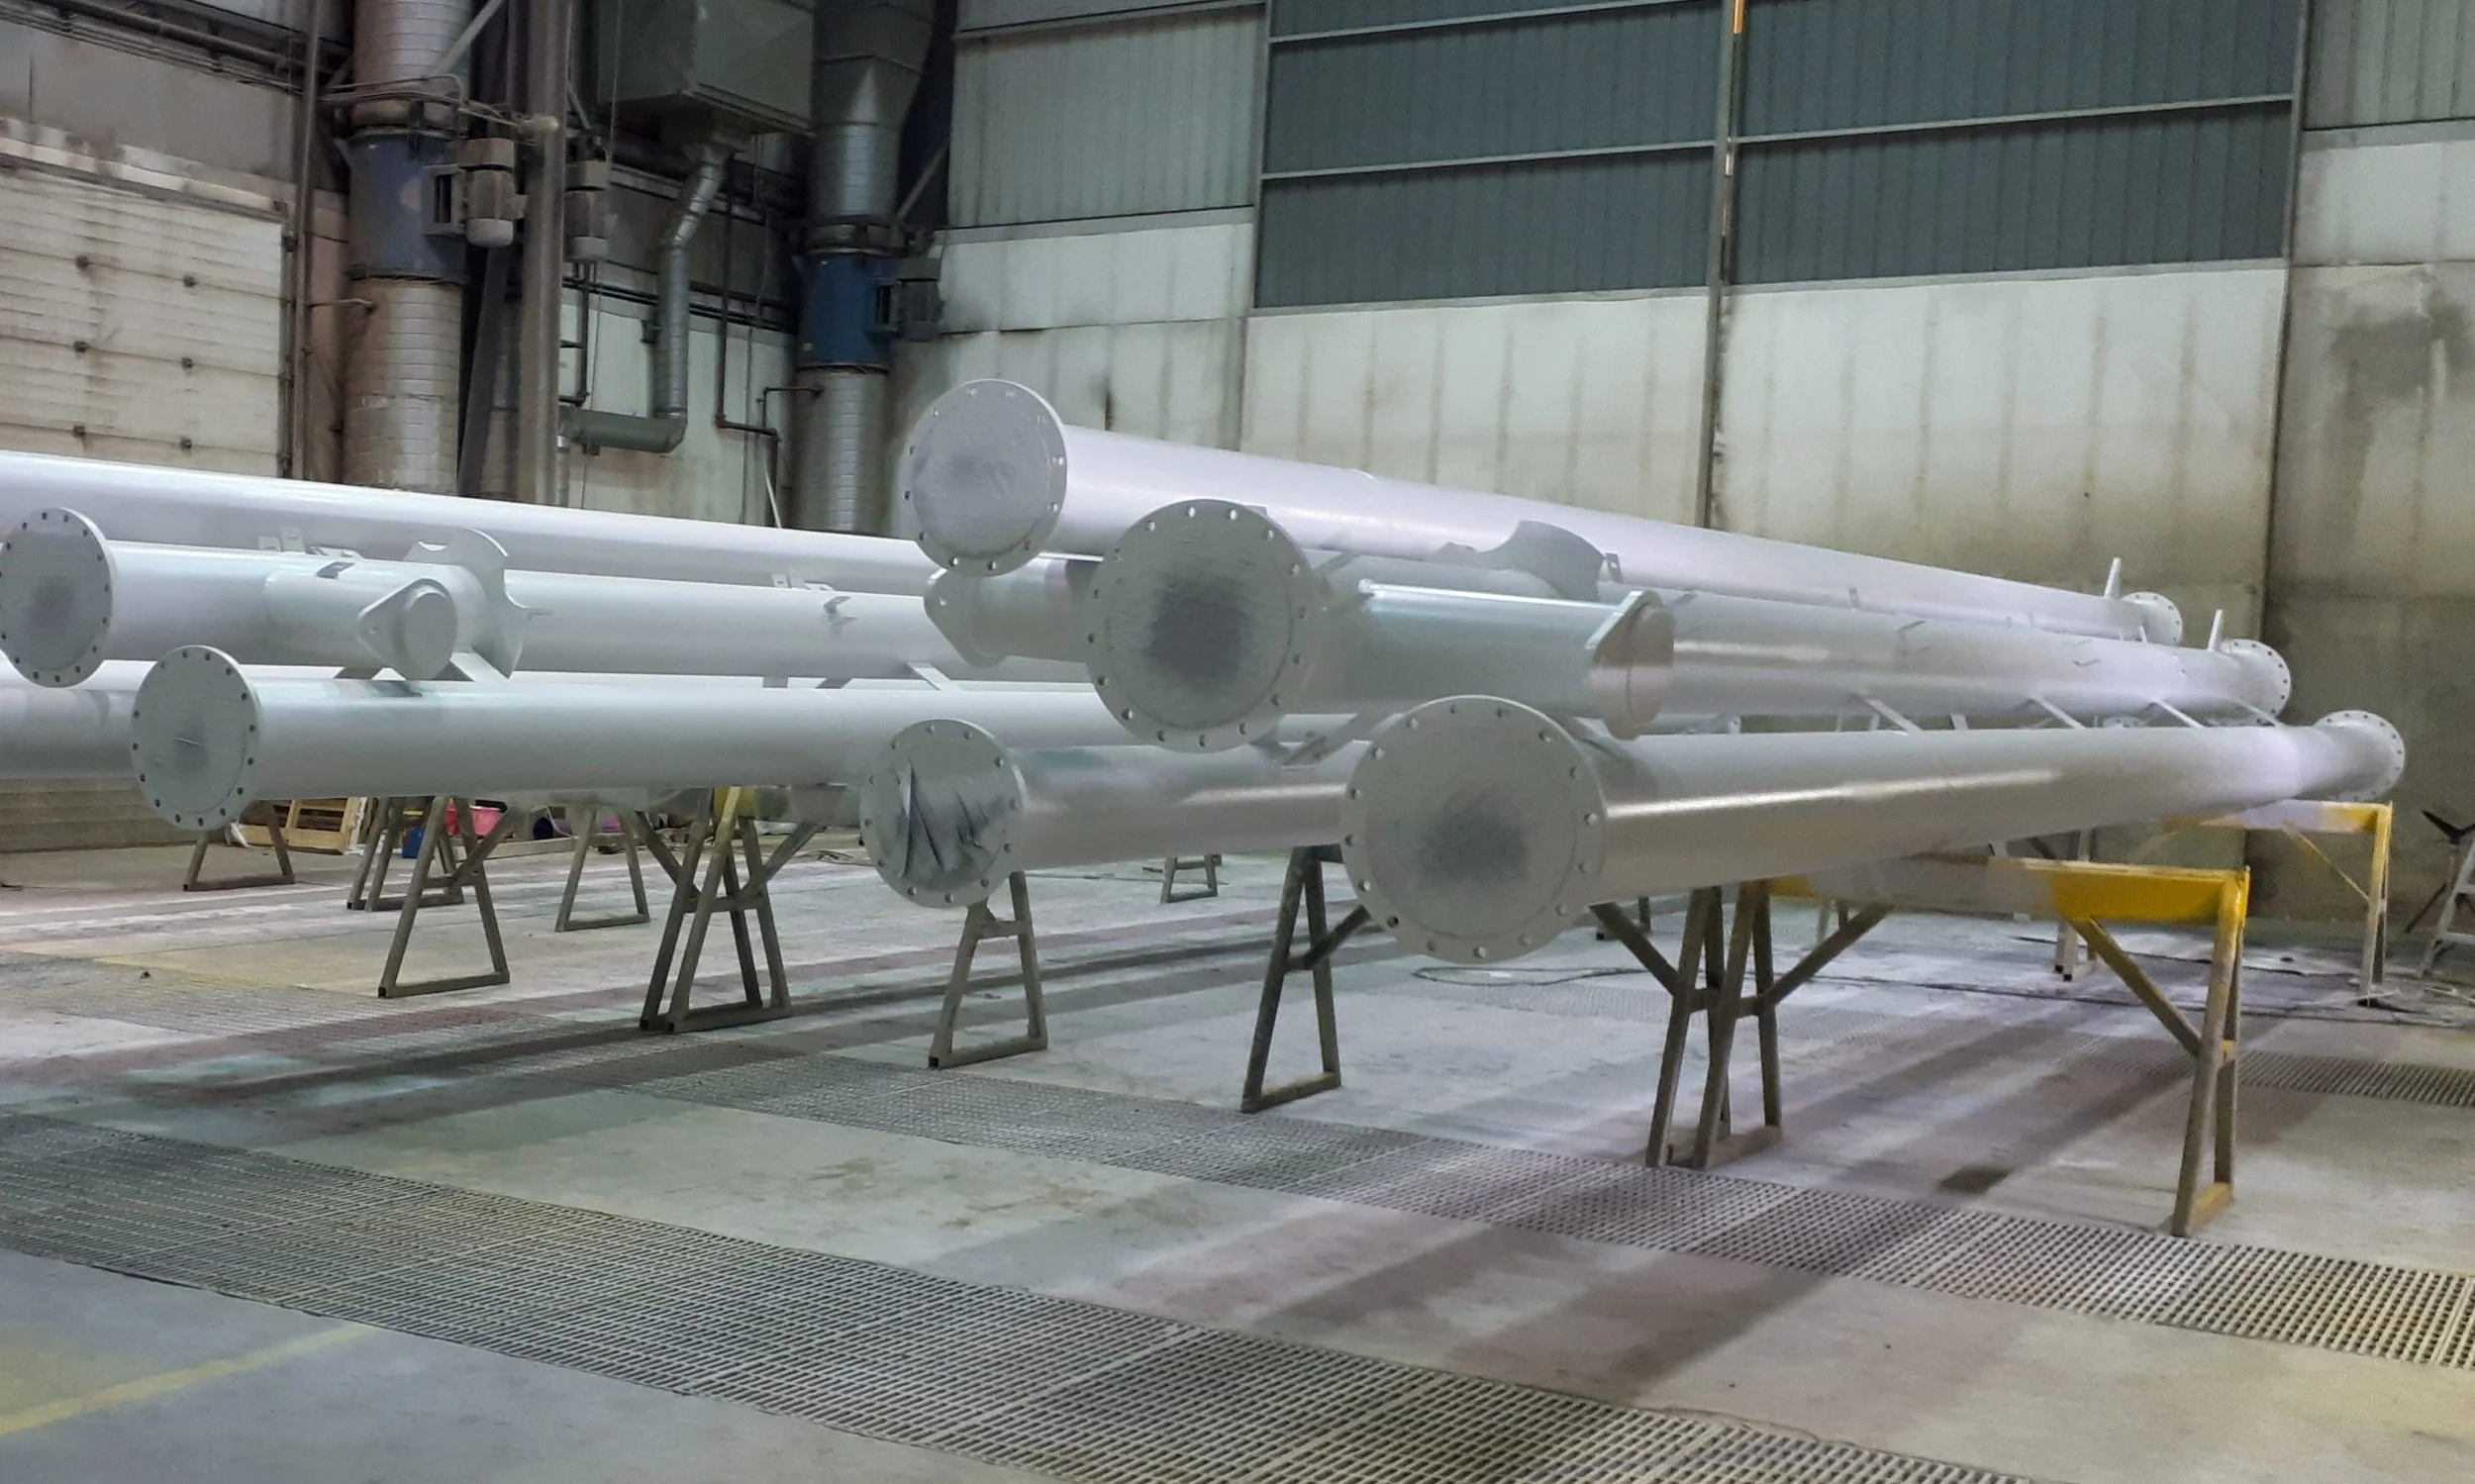
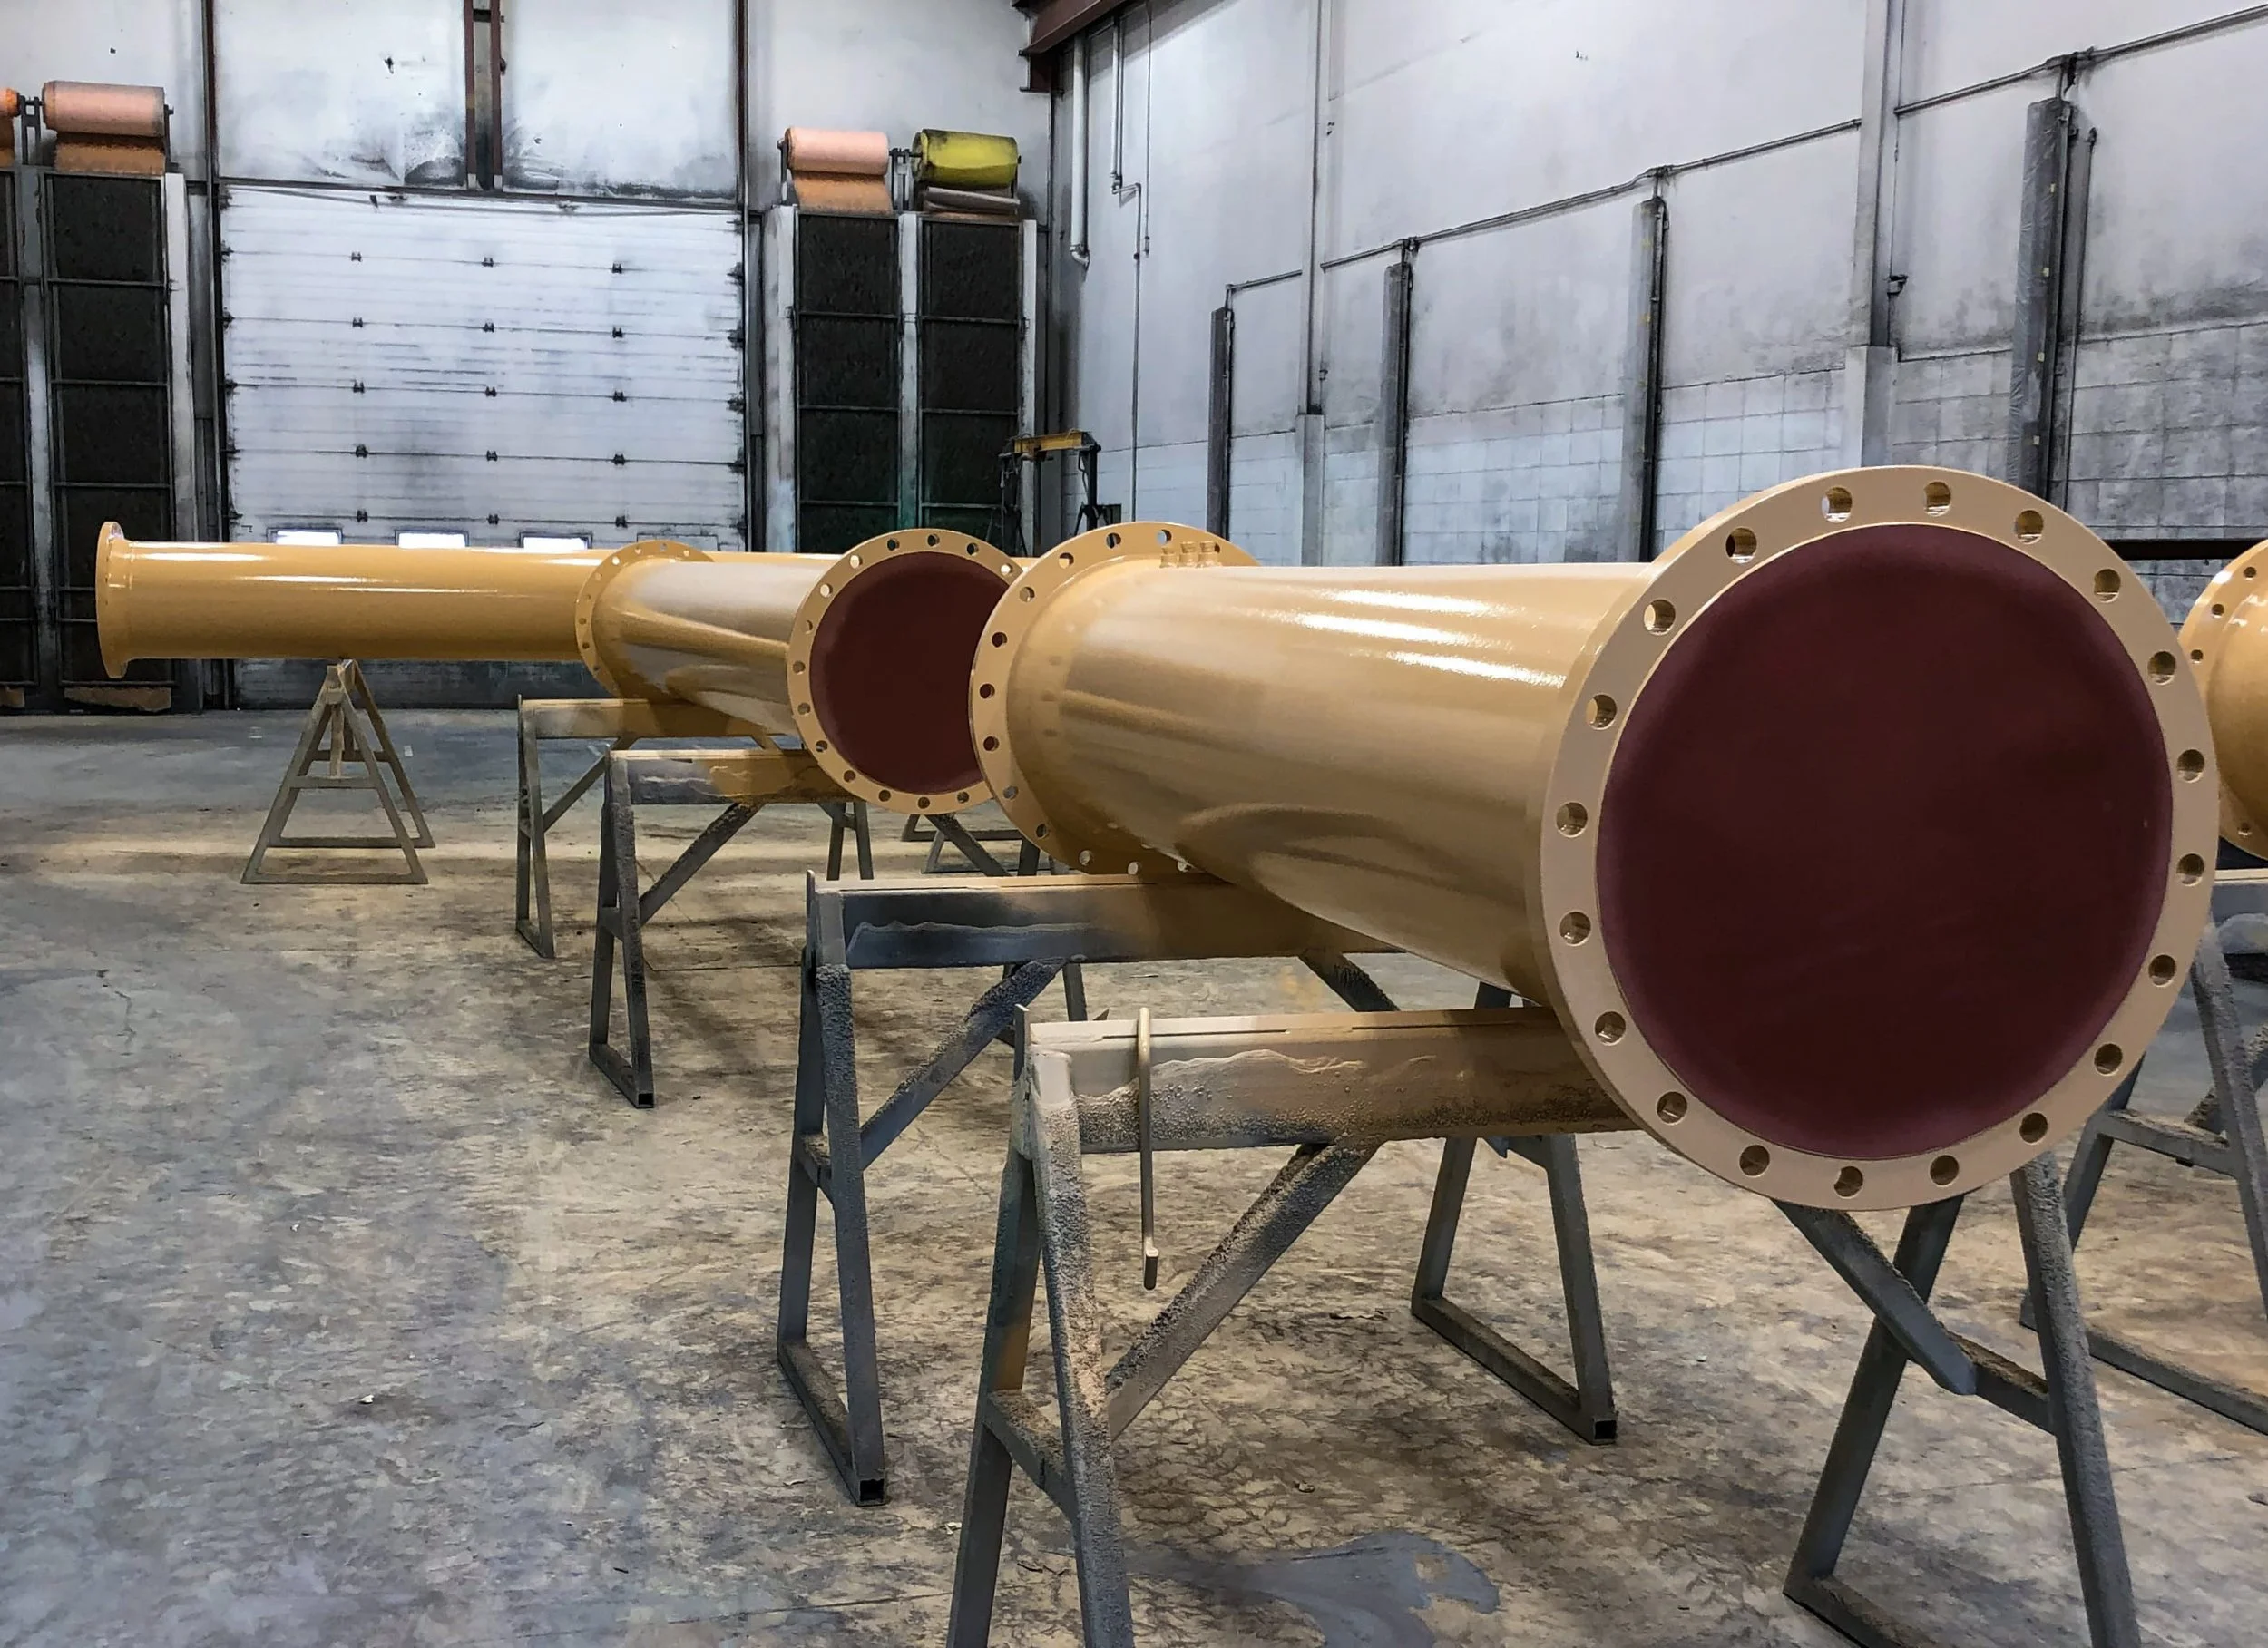
Pipeline Coatings
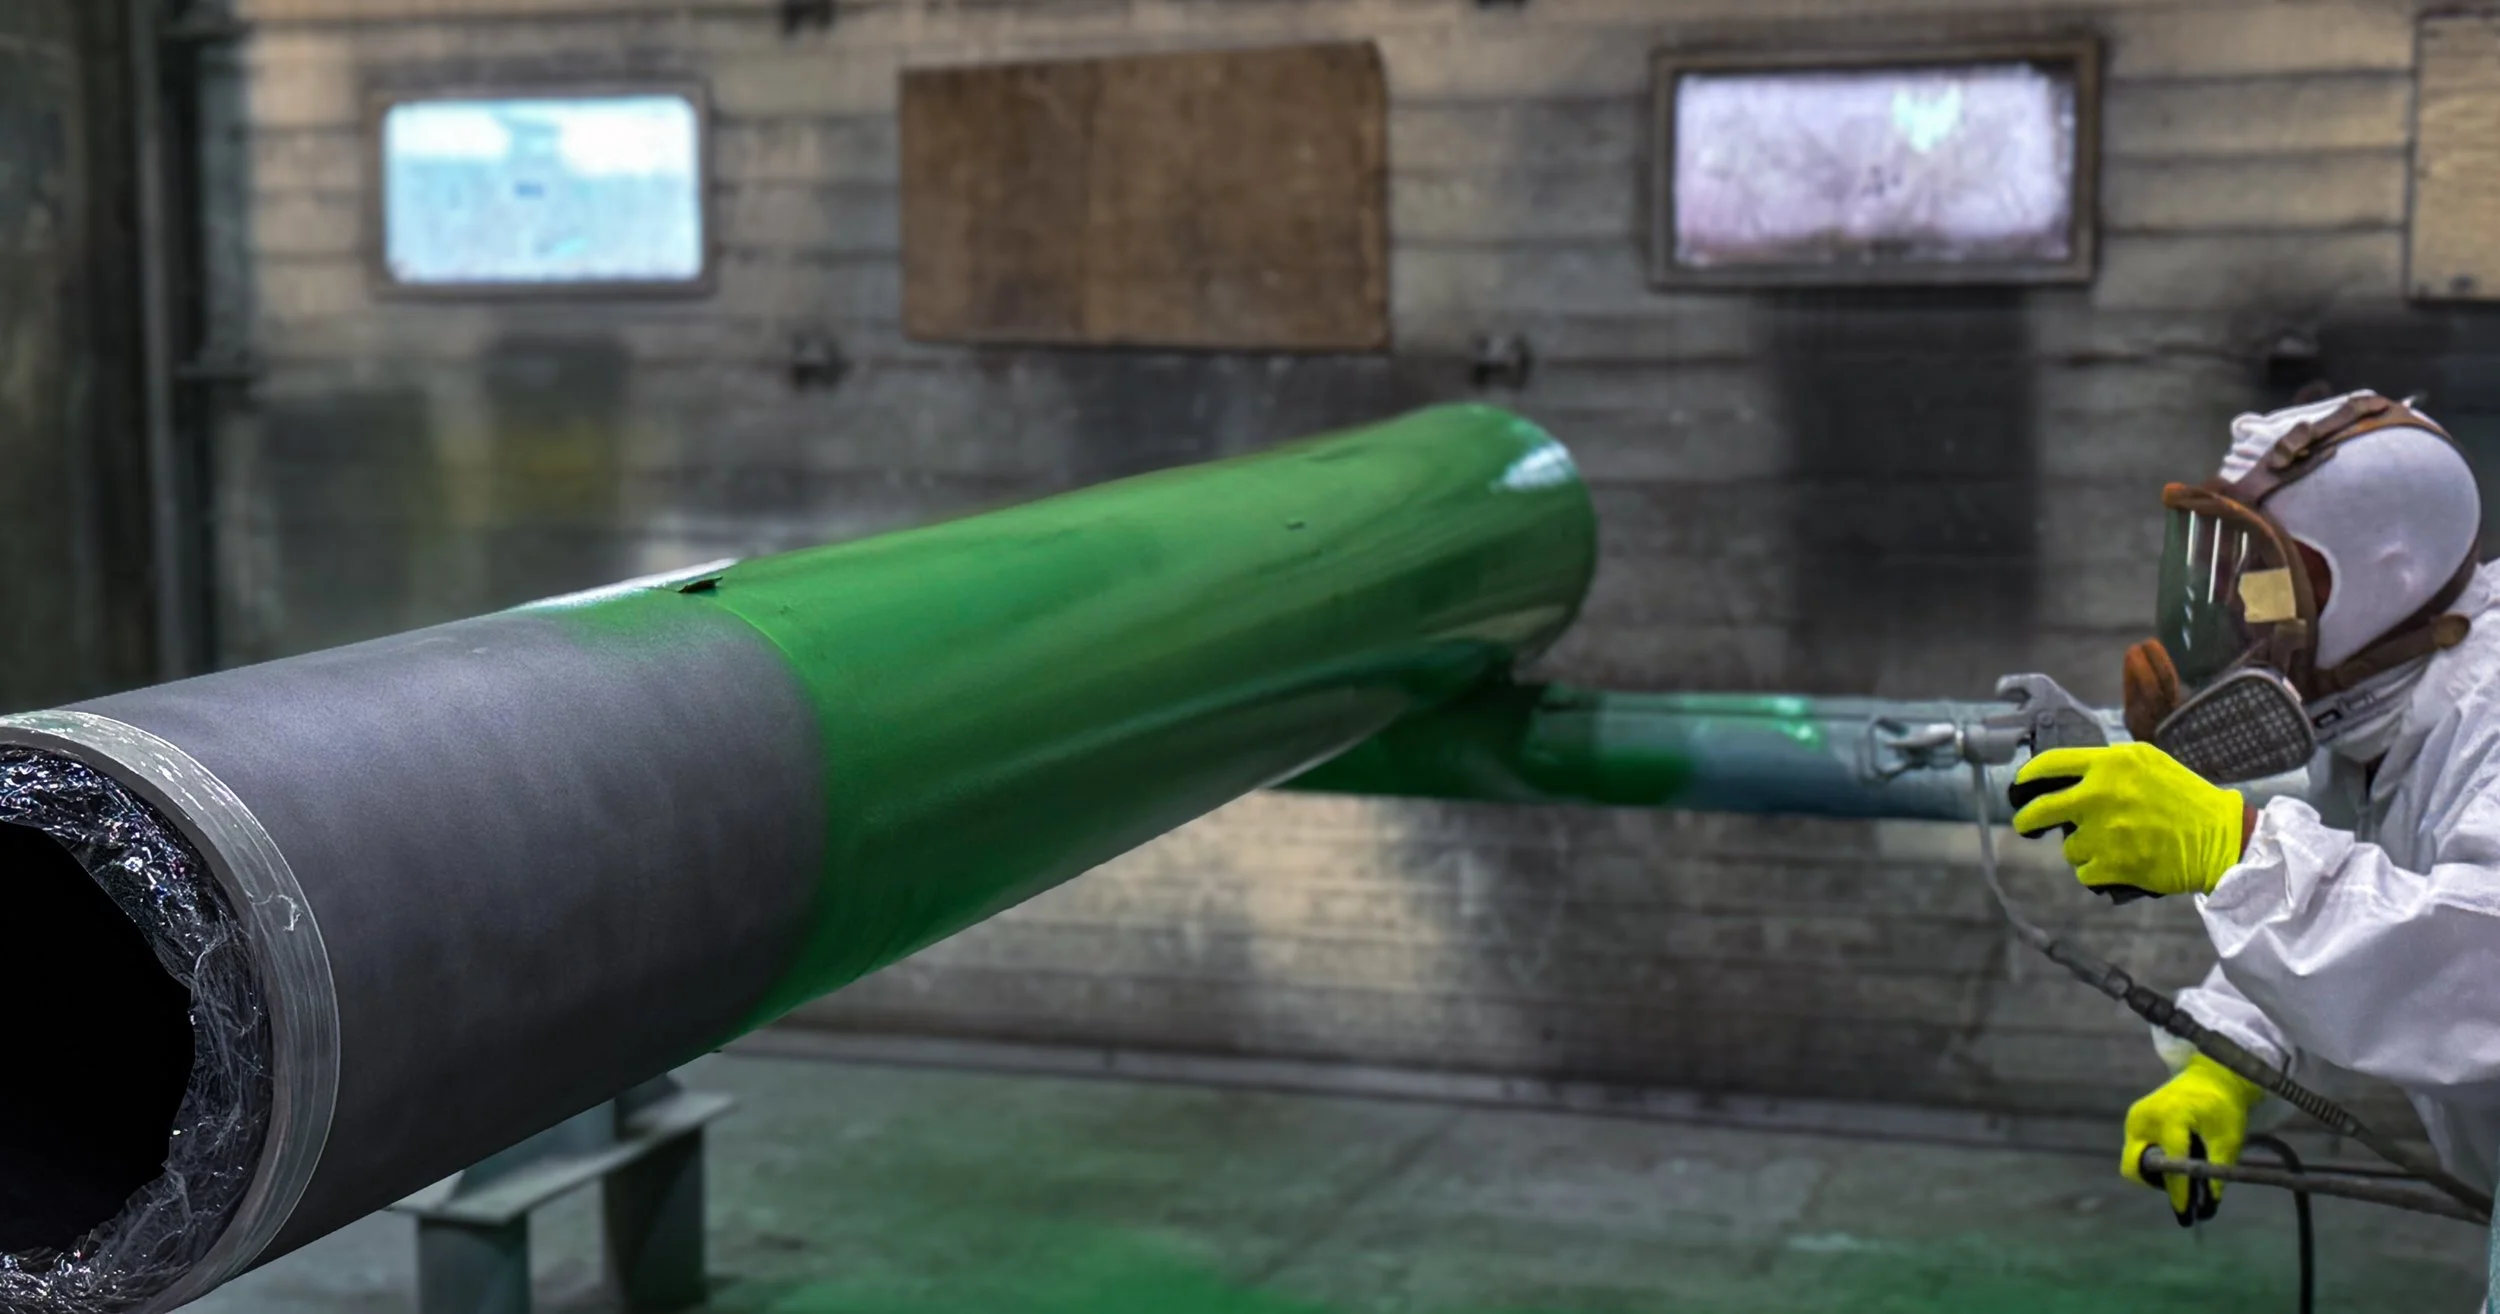
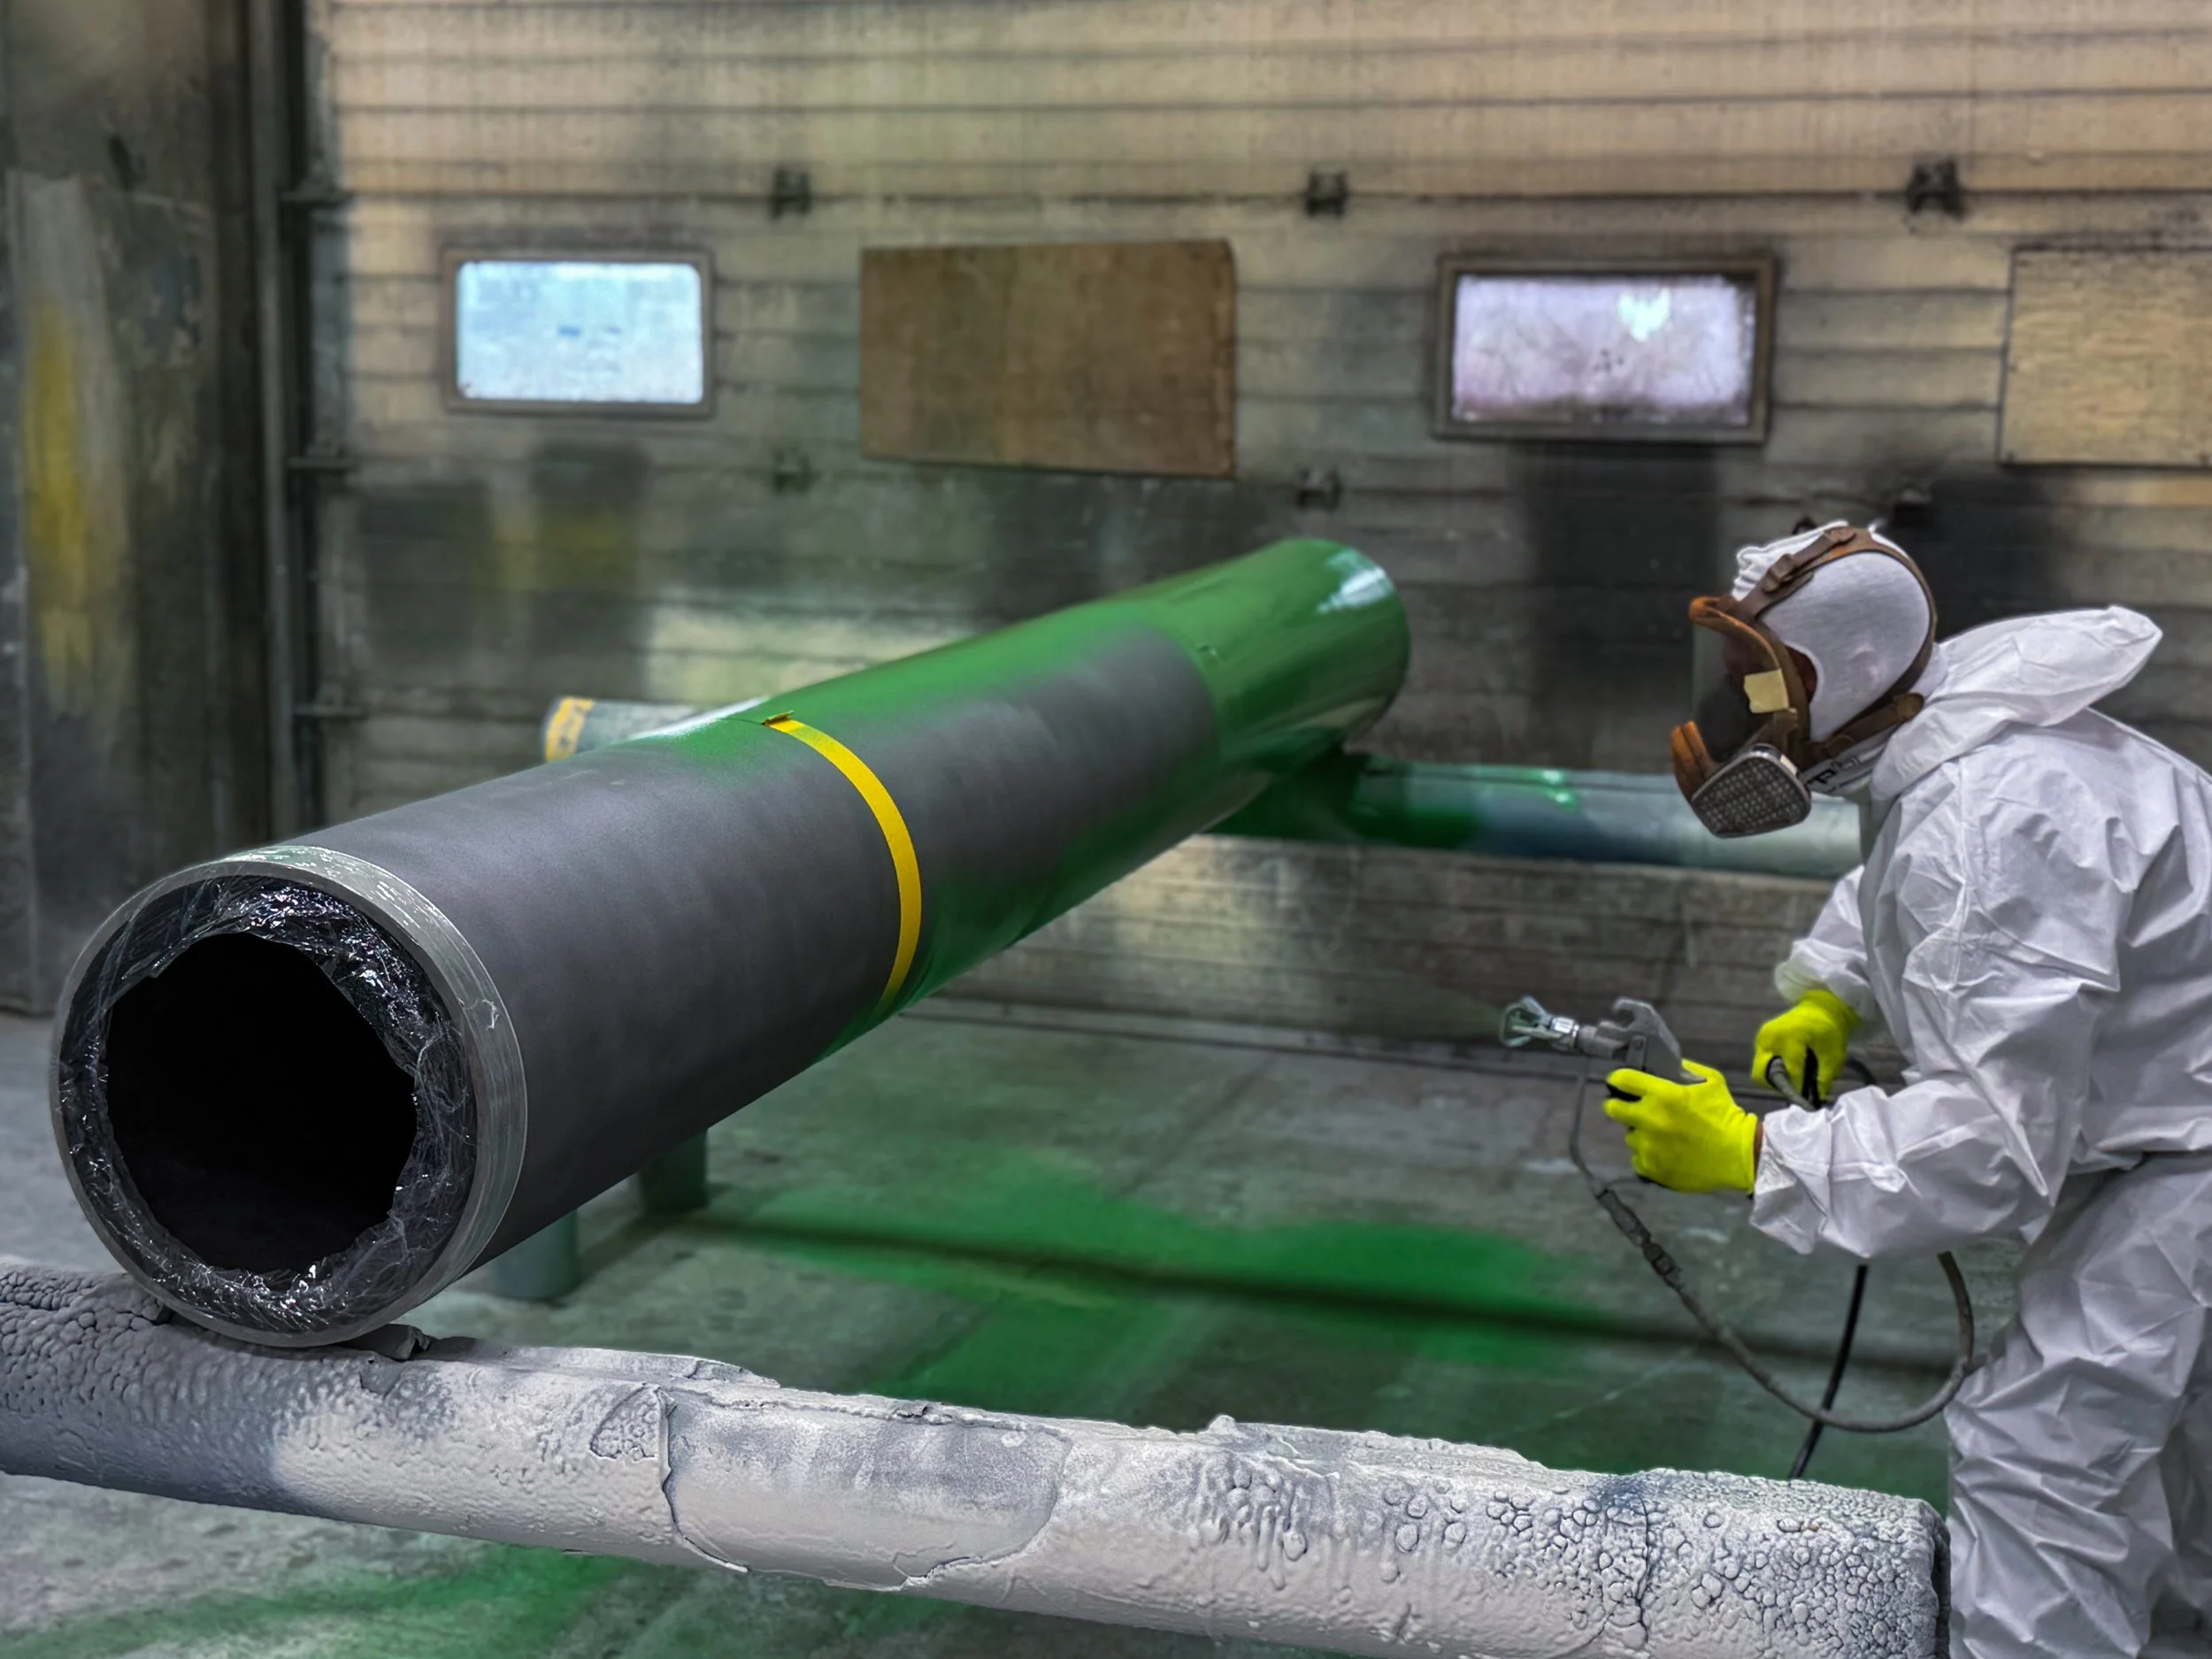
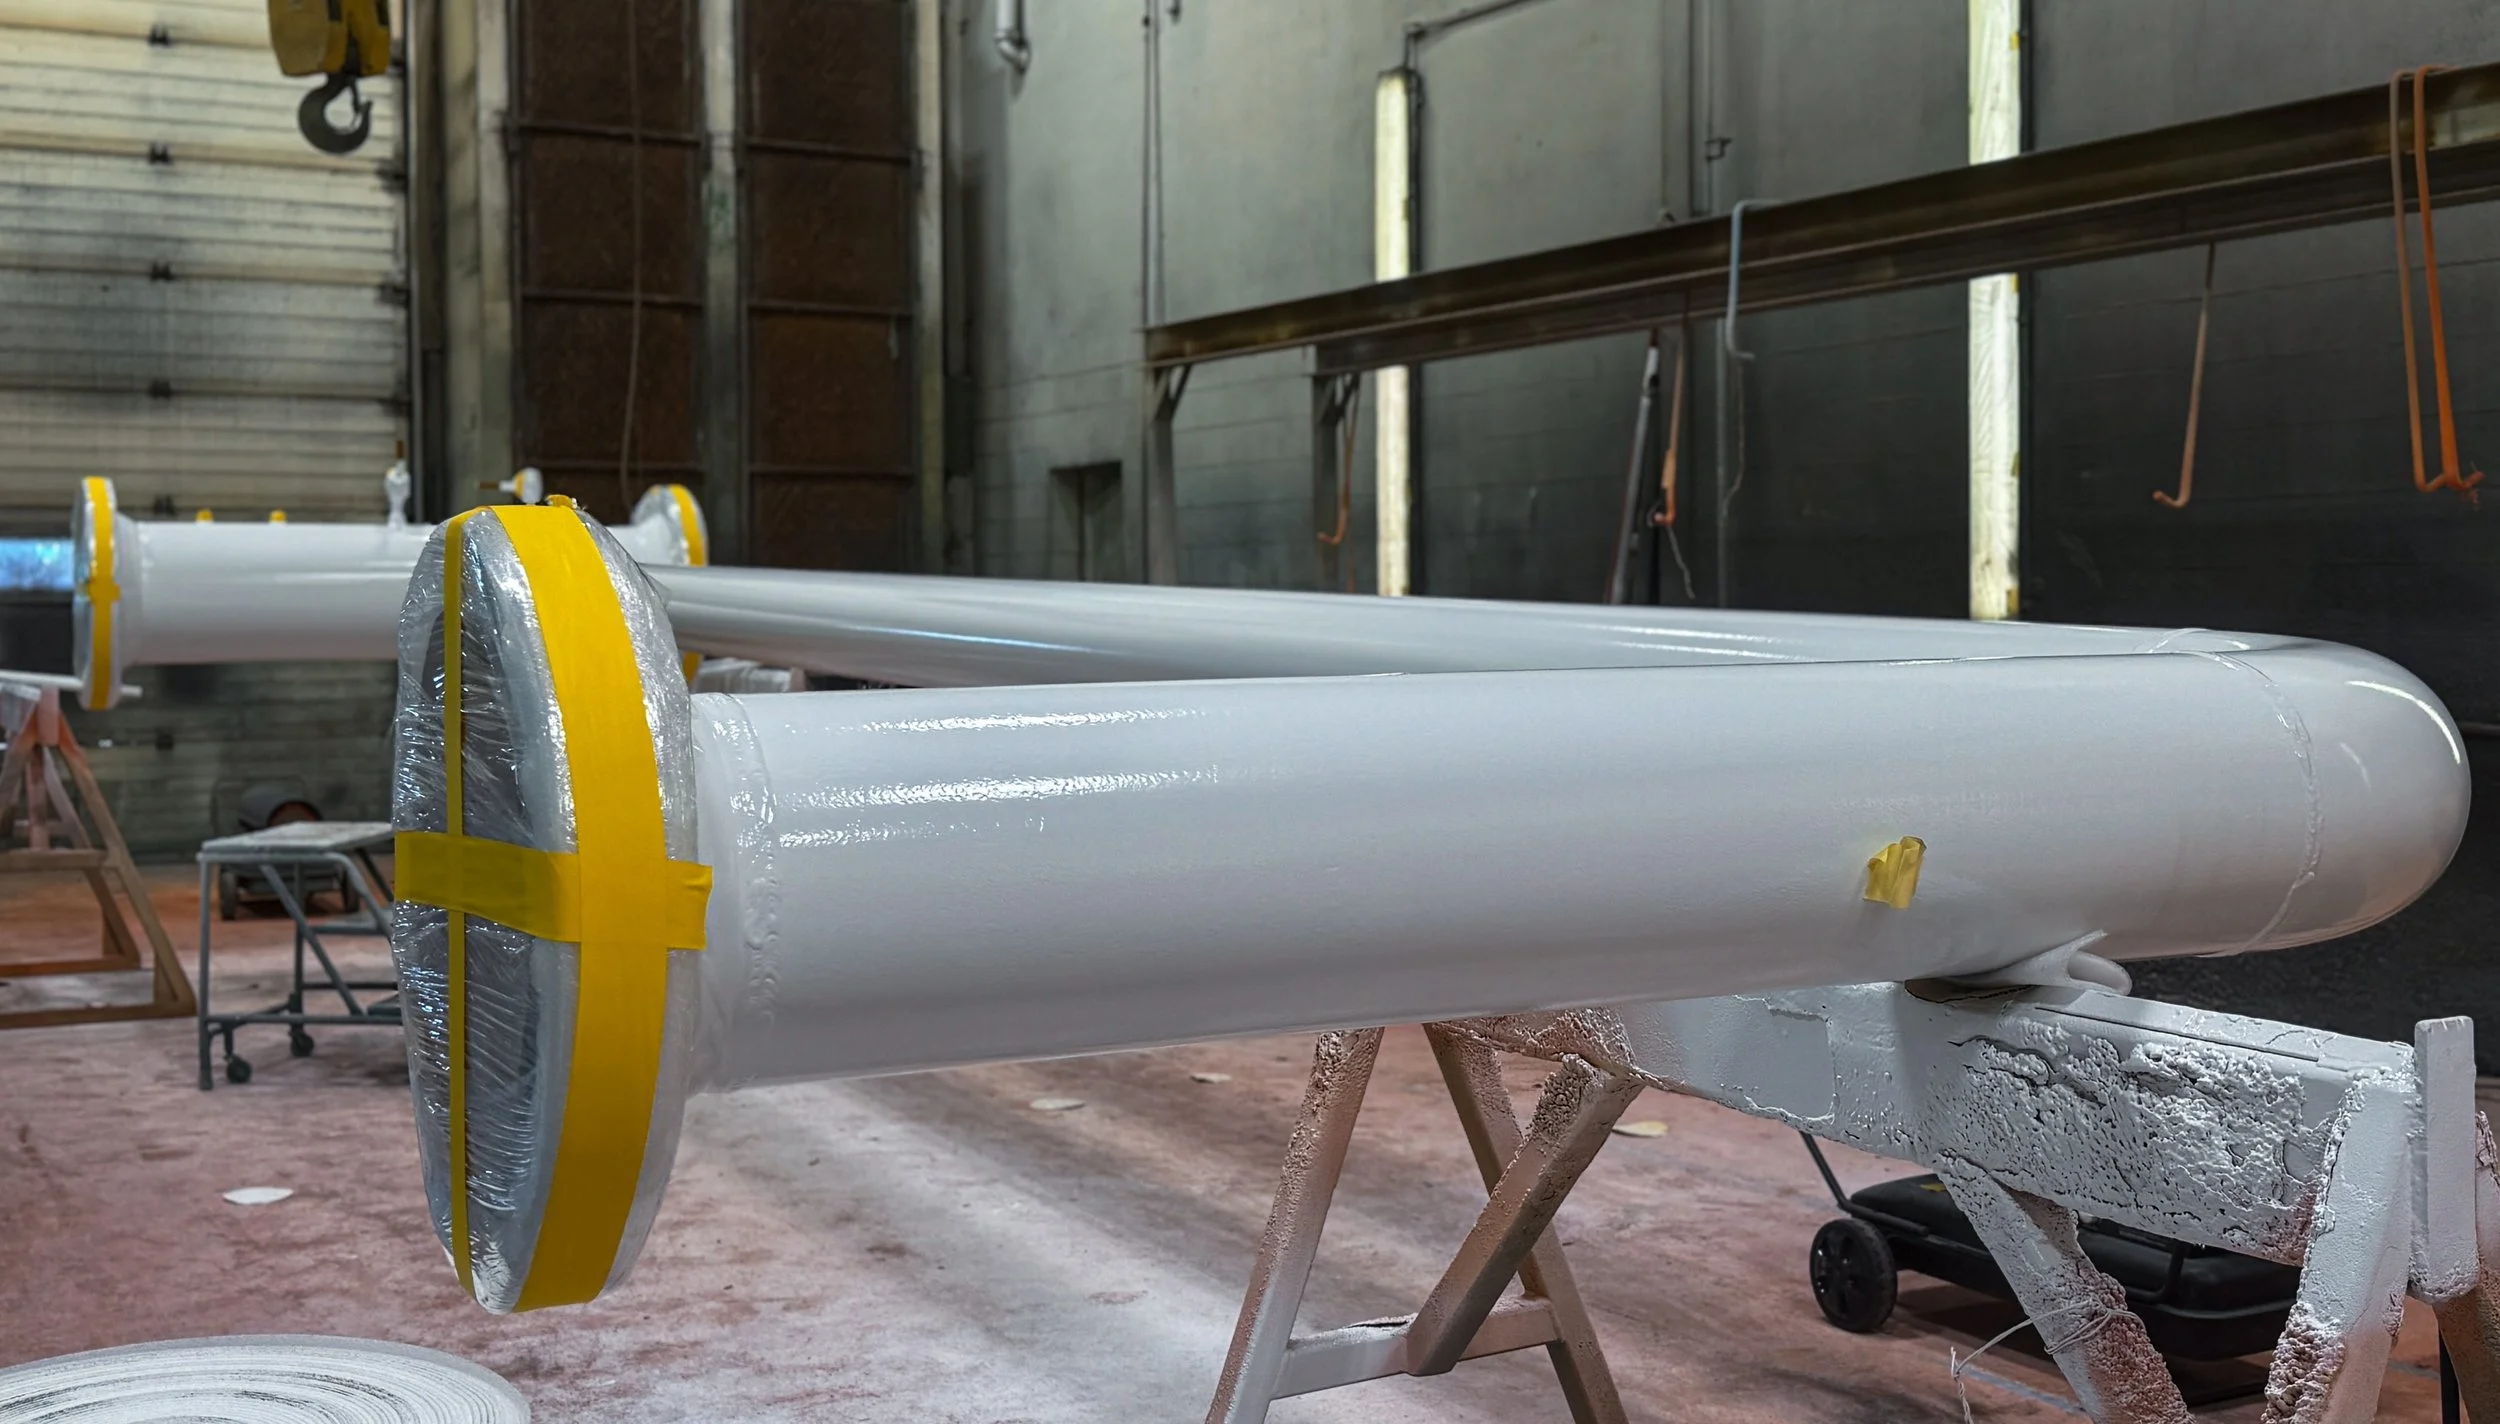
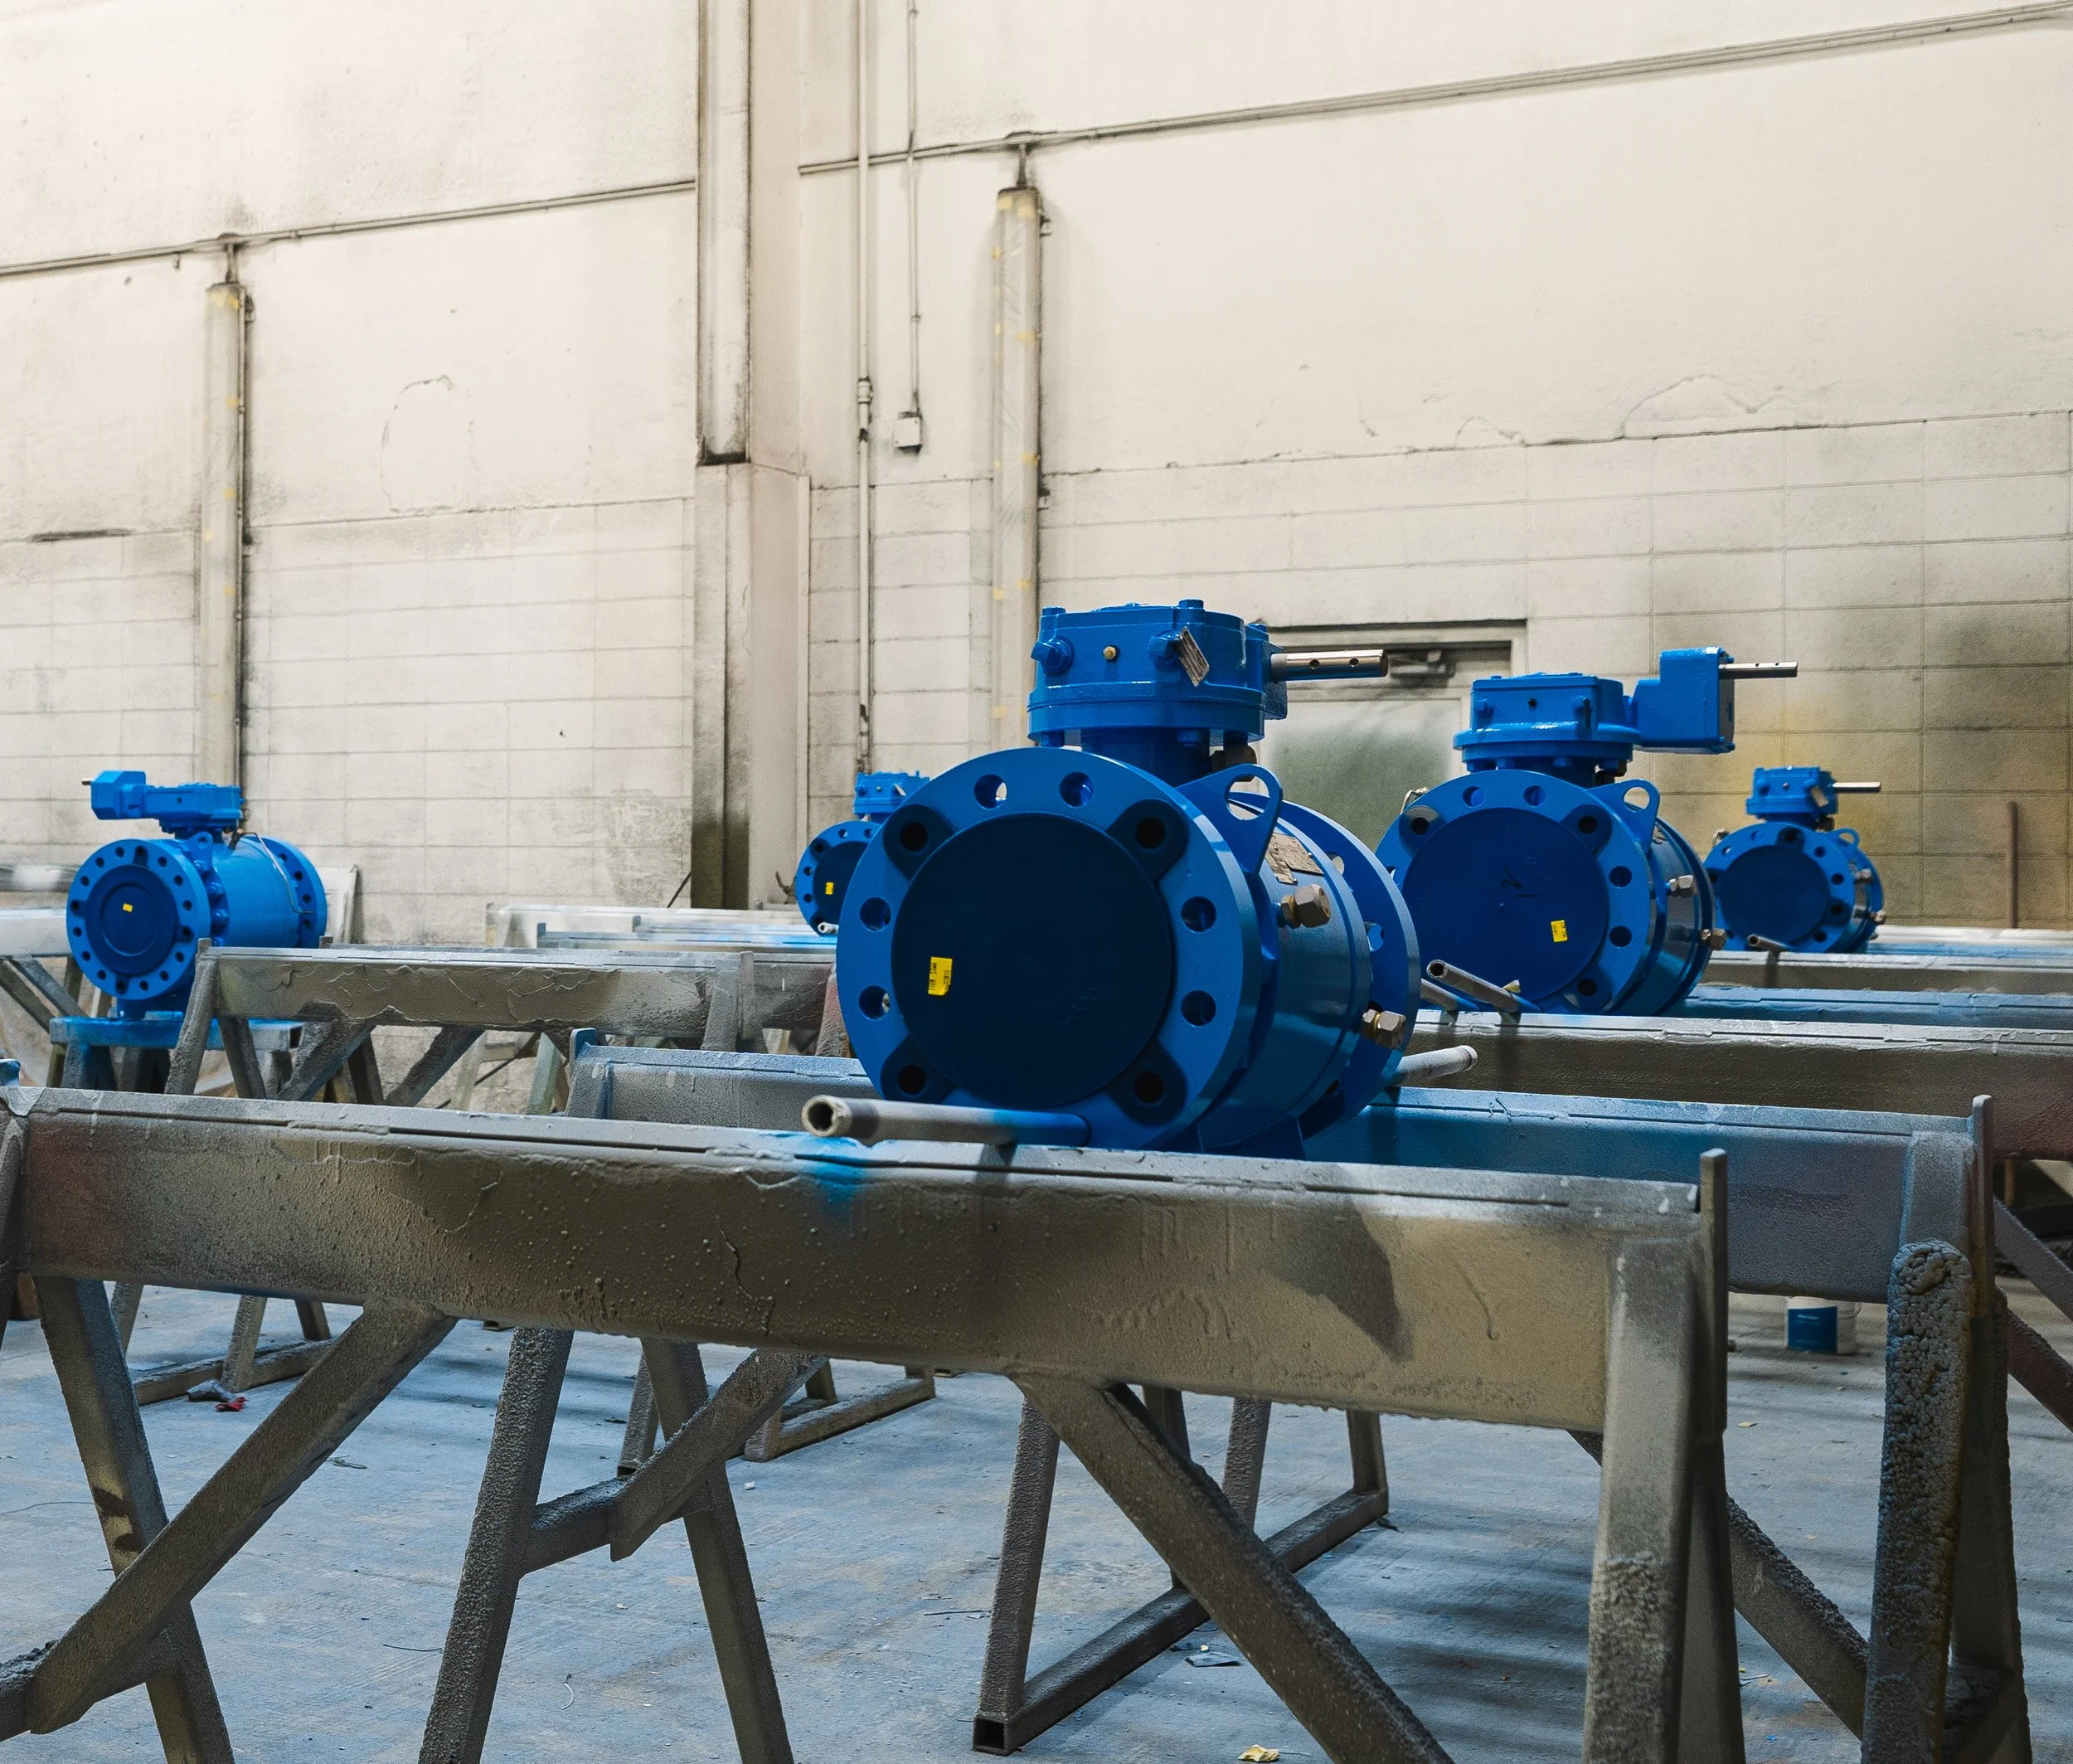
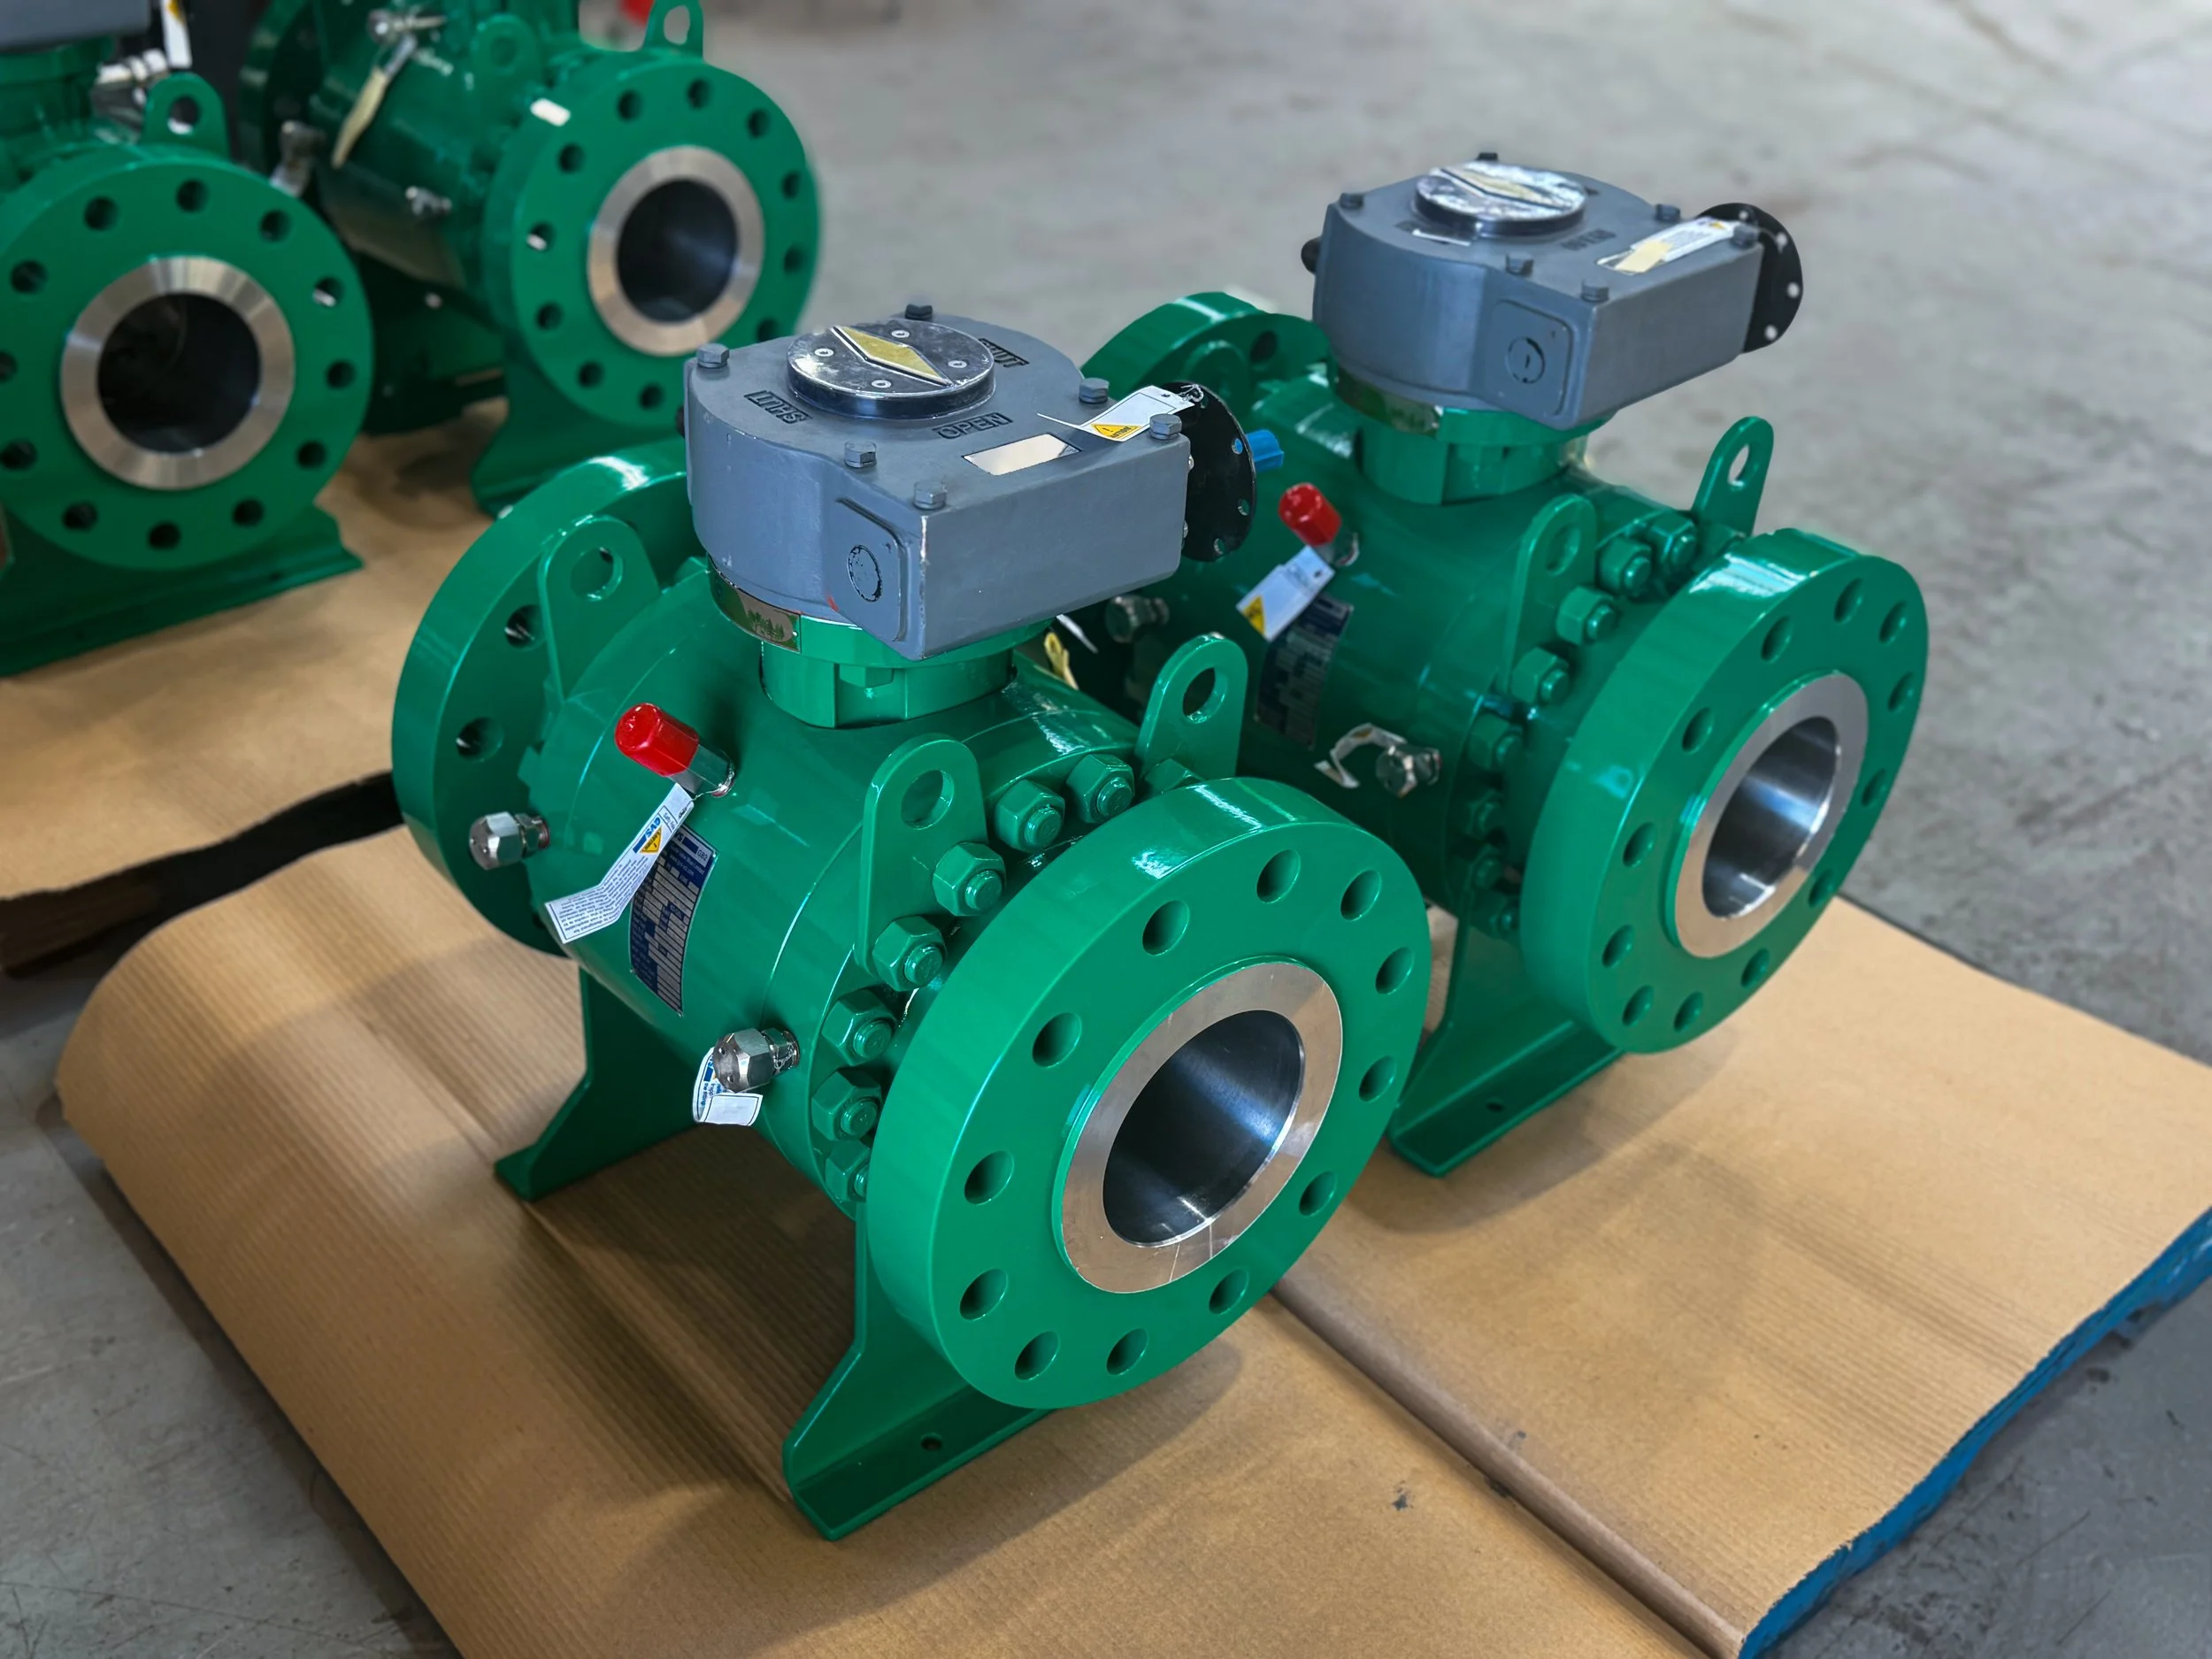
Extend the service life of your pipelines, spools, and flow control components with protective coatings applied to your exact specifications. Custom Coatings International’s NACE Level 2 & 3 certified inspectors carry out every inspection and test your specification calls for, with complete documentation to verify application quality. Learn more about our Denso Protal 7200, Fusion Bonded Epoxy (FBE), and polyurethane coating systems below.
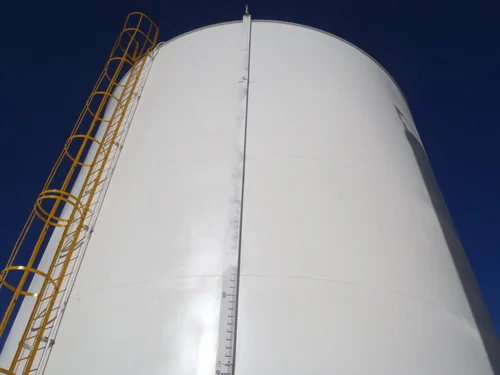
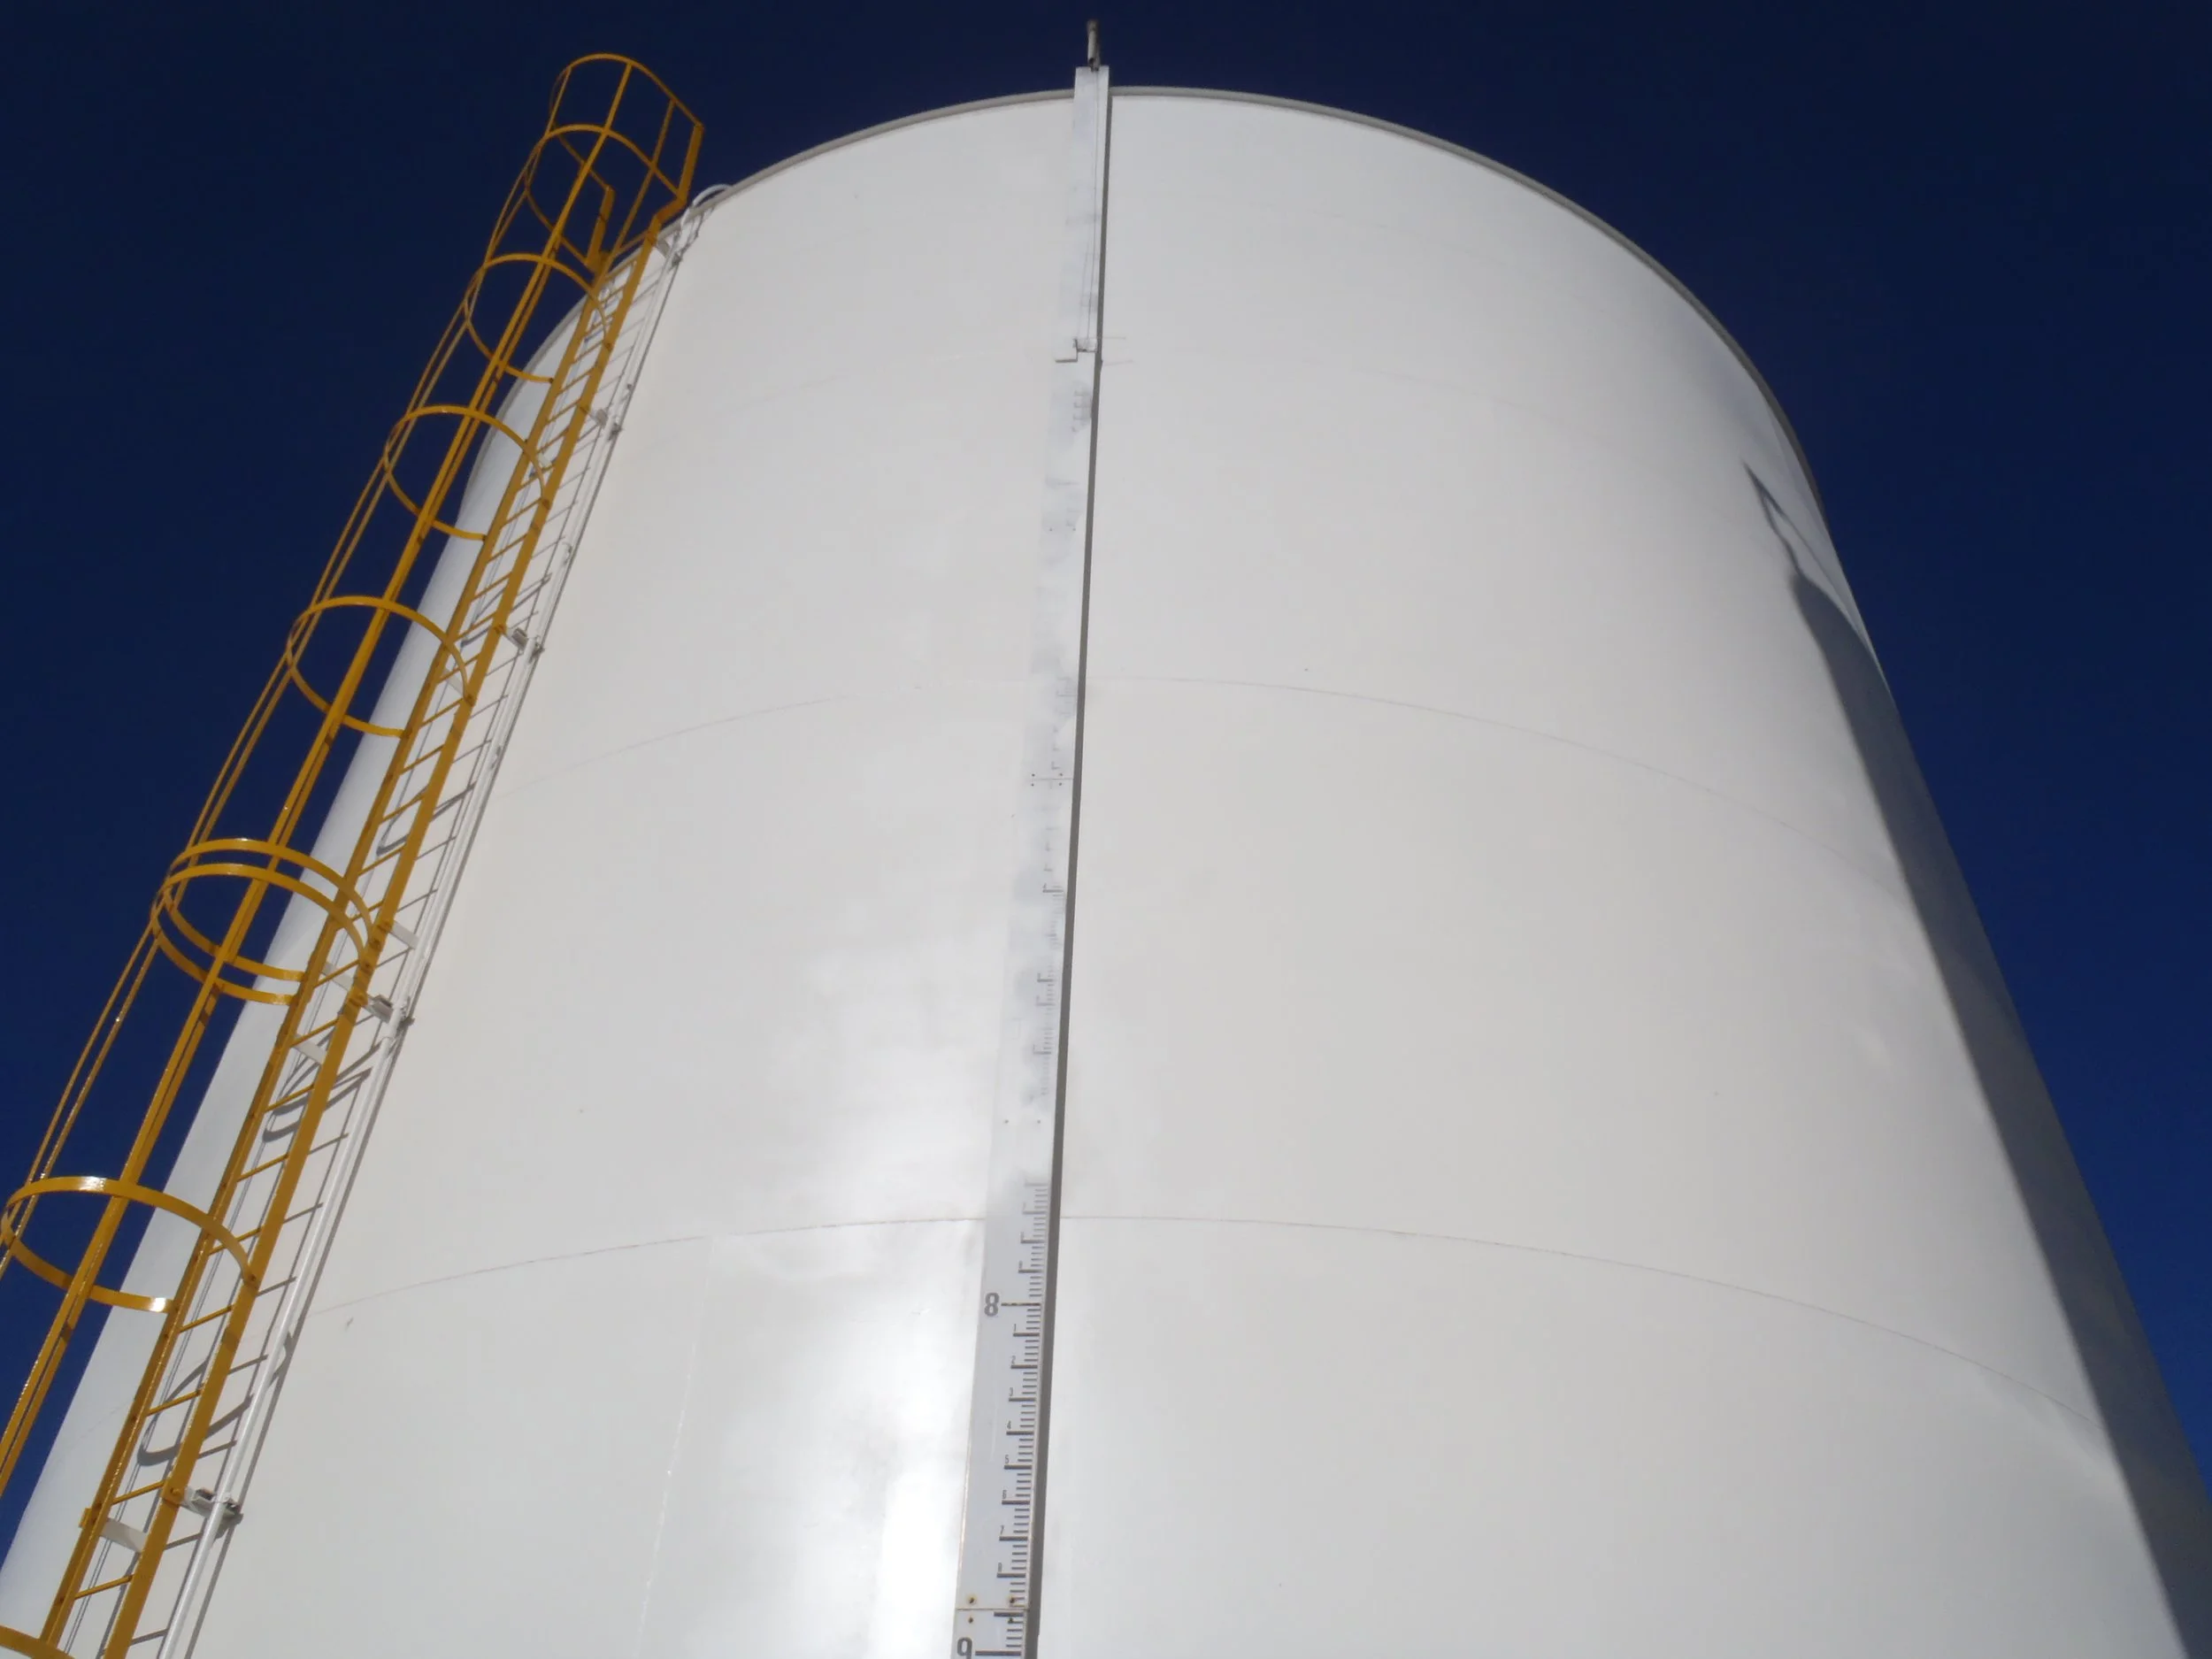
Tank Coatings & Lining
Custom Coatings International applies tank coatings and linings to your specifications for the oil and gas, water and wastewater, chemical storage, and agricultural industries across Alberta. Every project is inspected and tested as your specification requires by our NACE Level 2 & 3 certified inspectors, with full documentation to verify quality, protecting your tanks from corrosion and contamination.
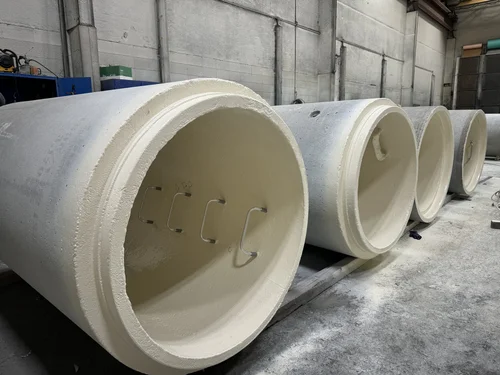
Concrete Coating
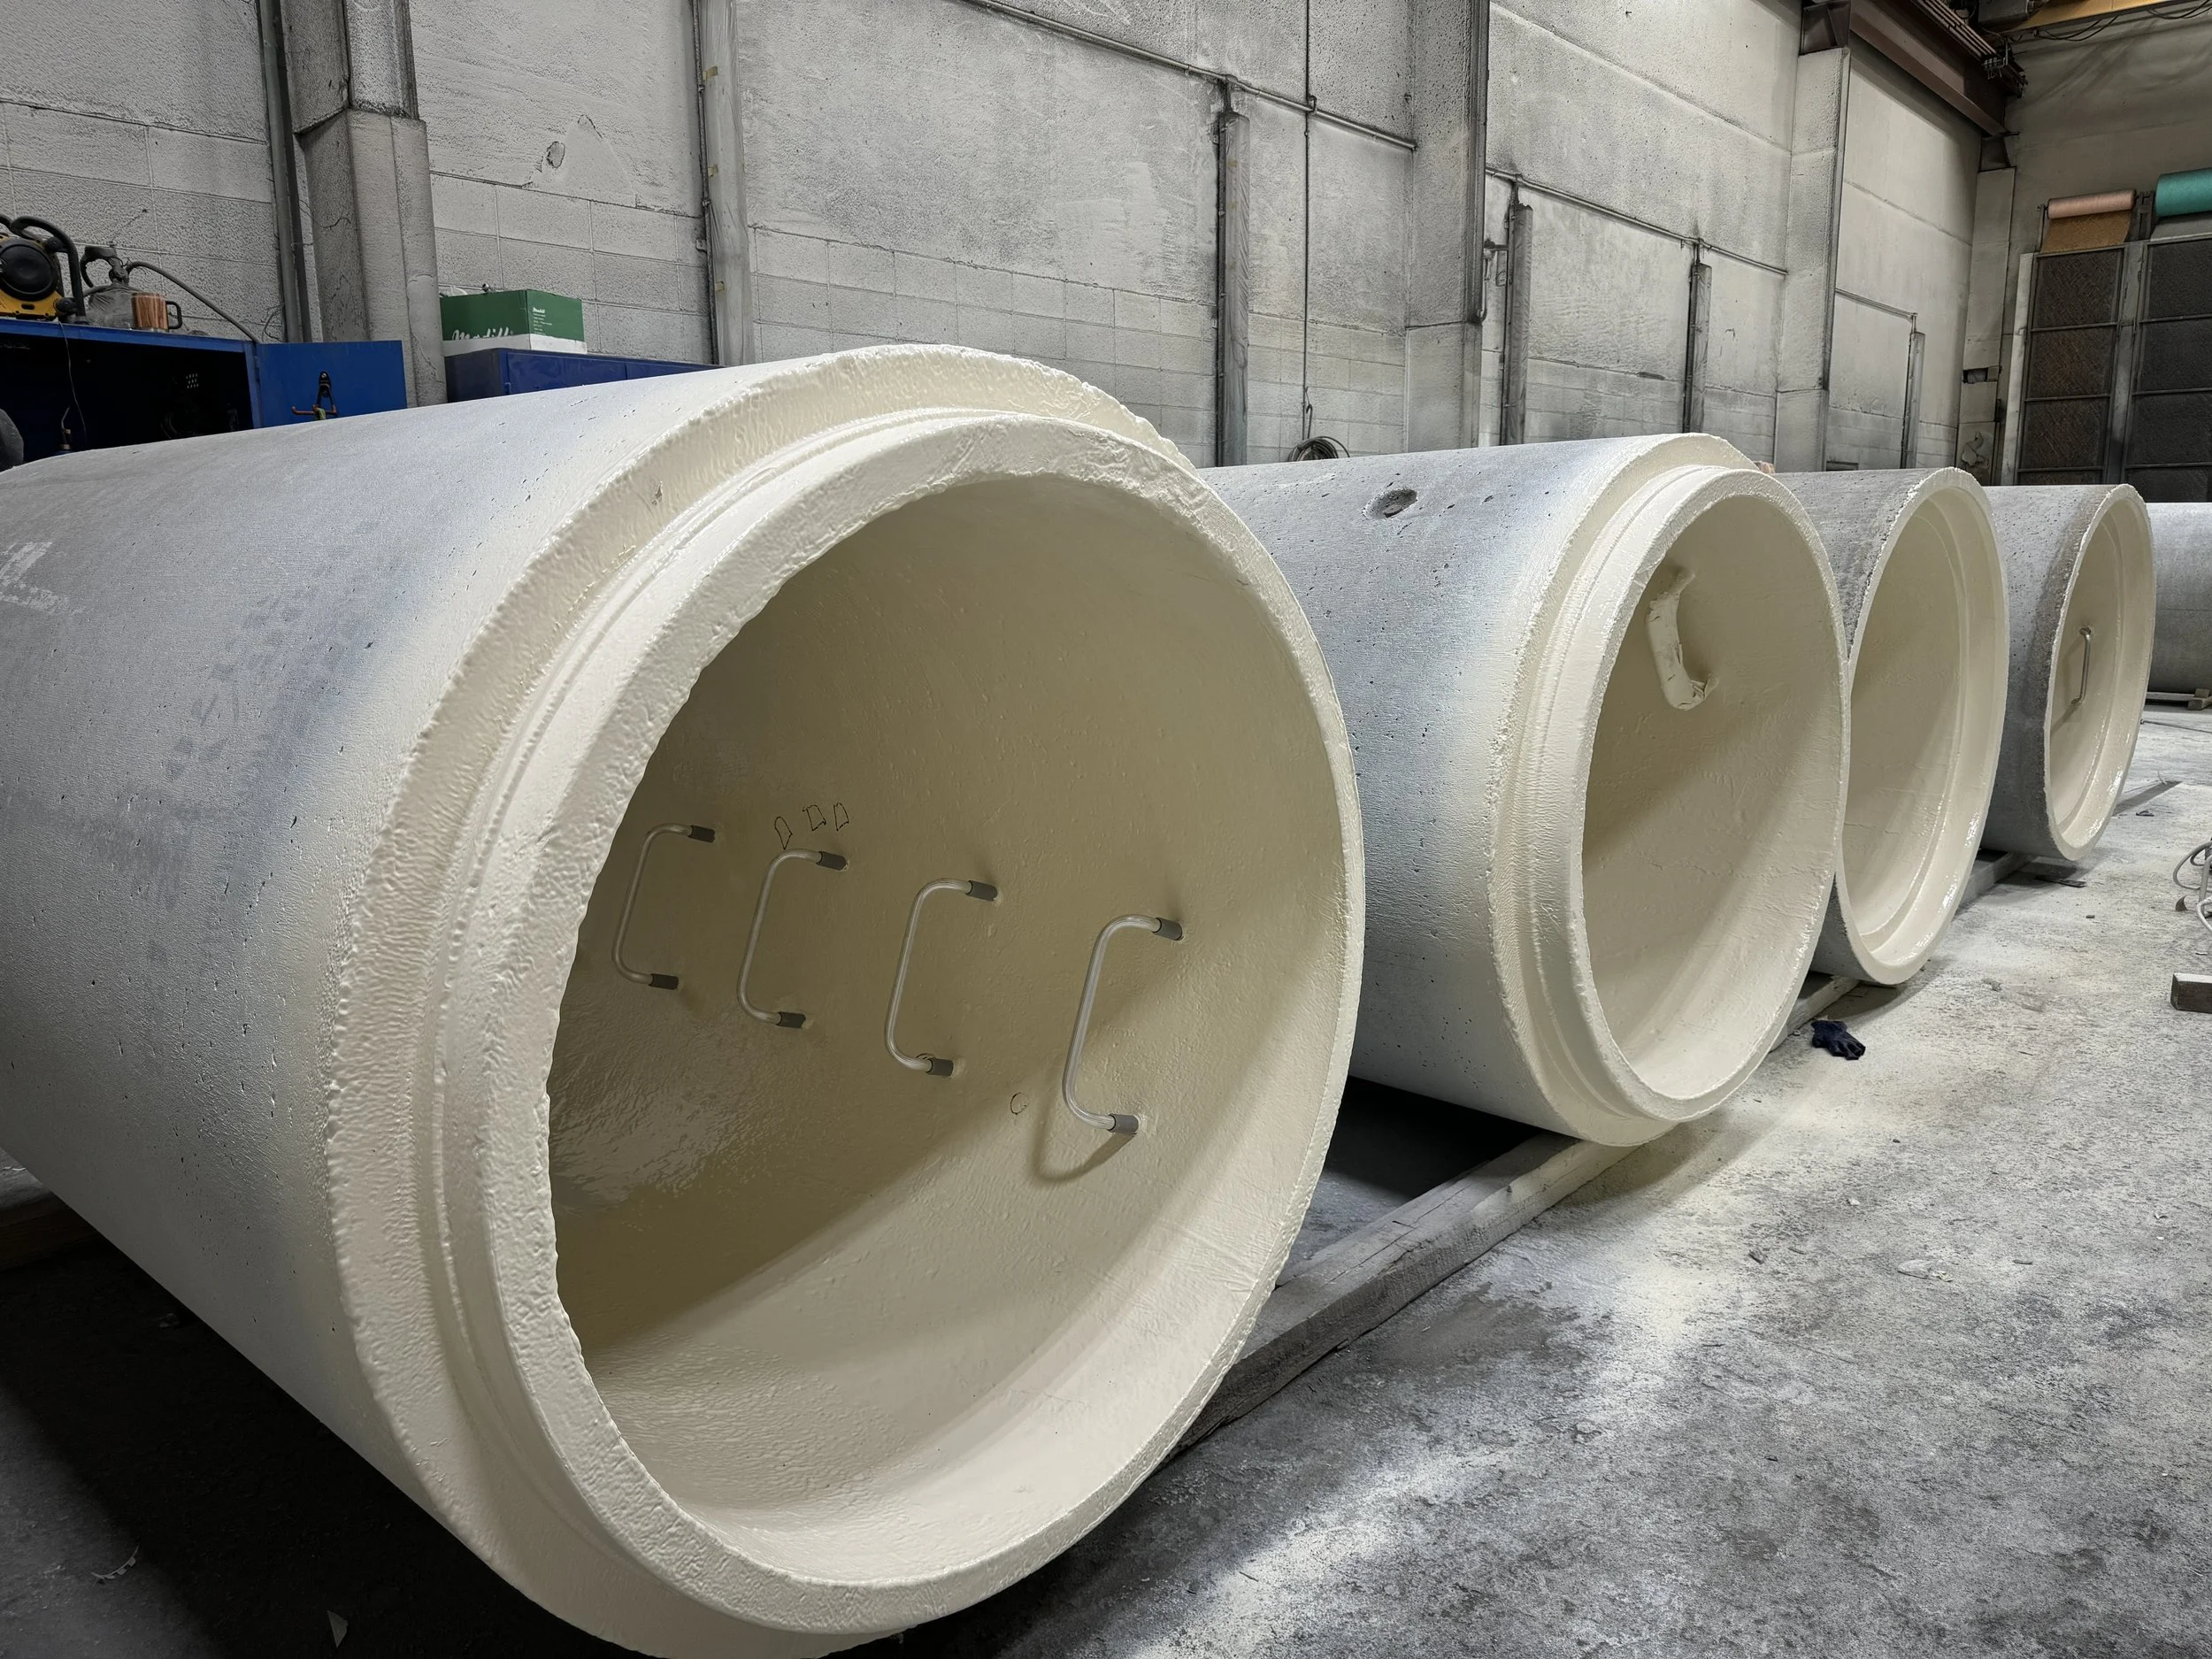
Custom Coatings International applies protective coating systems to precast concrete to your specifications, protecting it from abrasion, impact, moisture, and chemical exposure. Serving water treatment, civil infrastructure, oil and gas, and agricultural applications, our coatings help preserve structural integrity and extend service life. We apply epoxy, polyurethane, and polyaspartic coating systems as well as acrylic sealers, so each structure is protected according to its service environment.
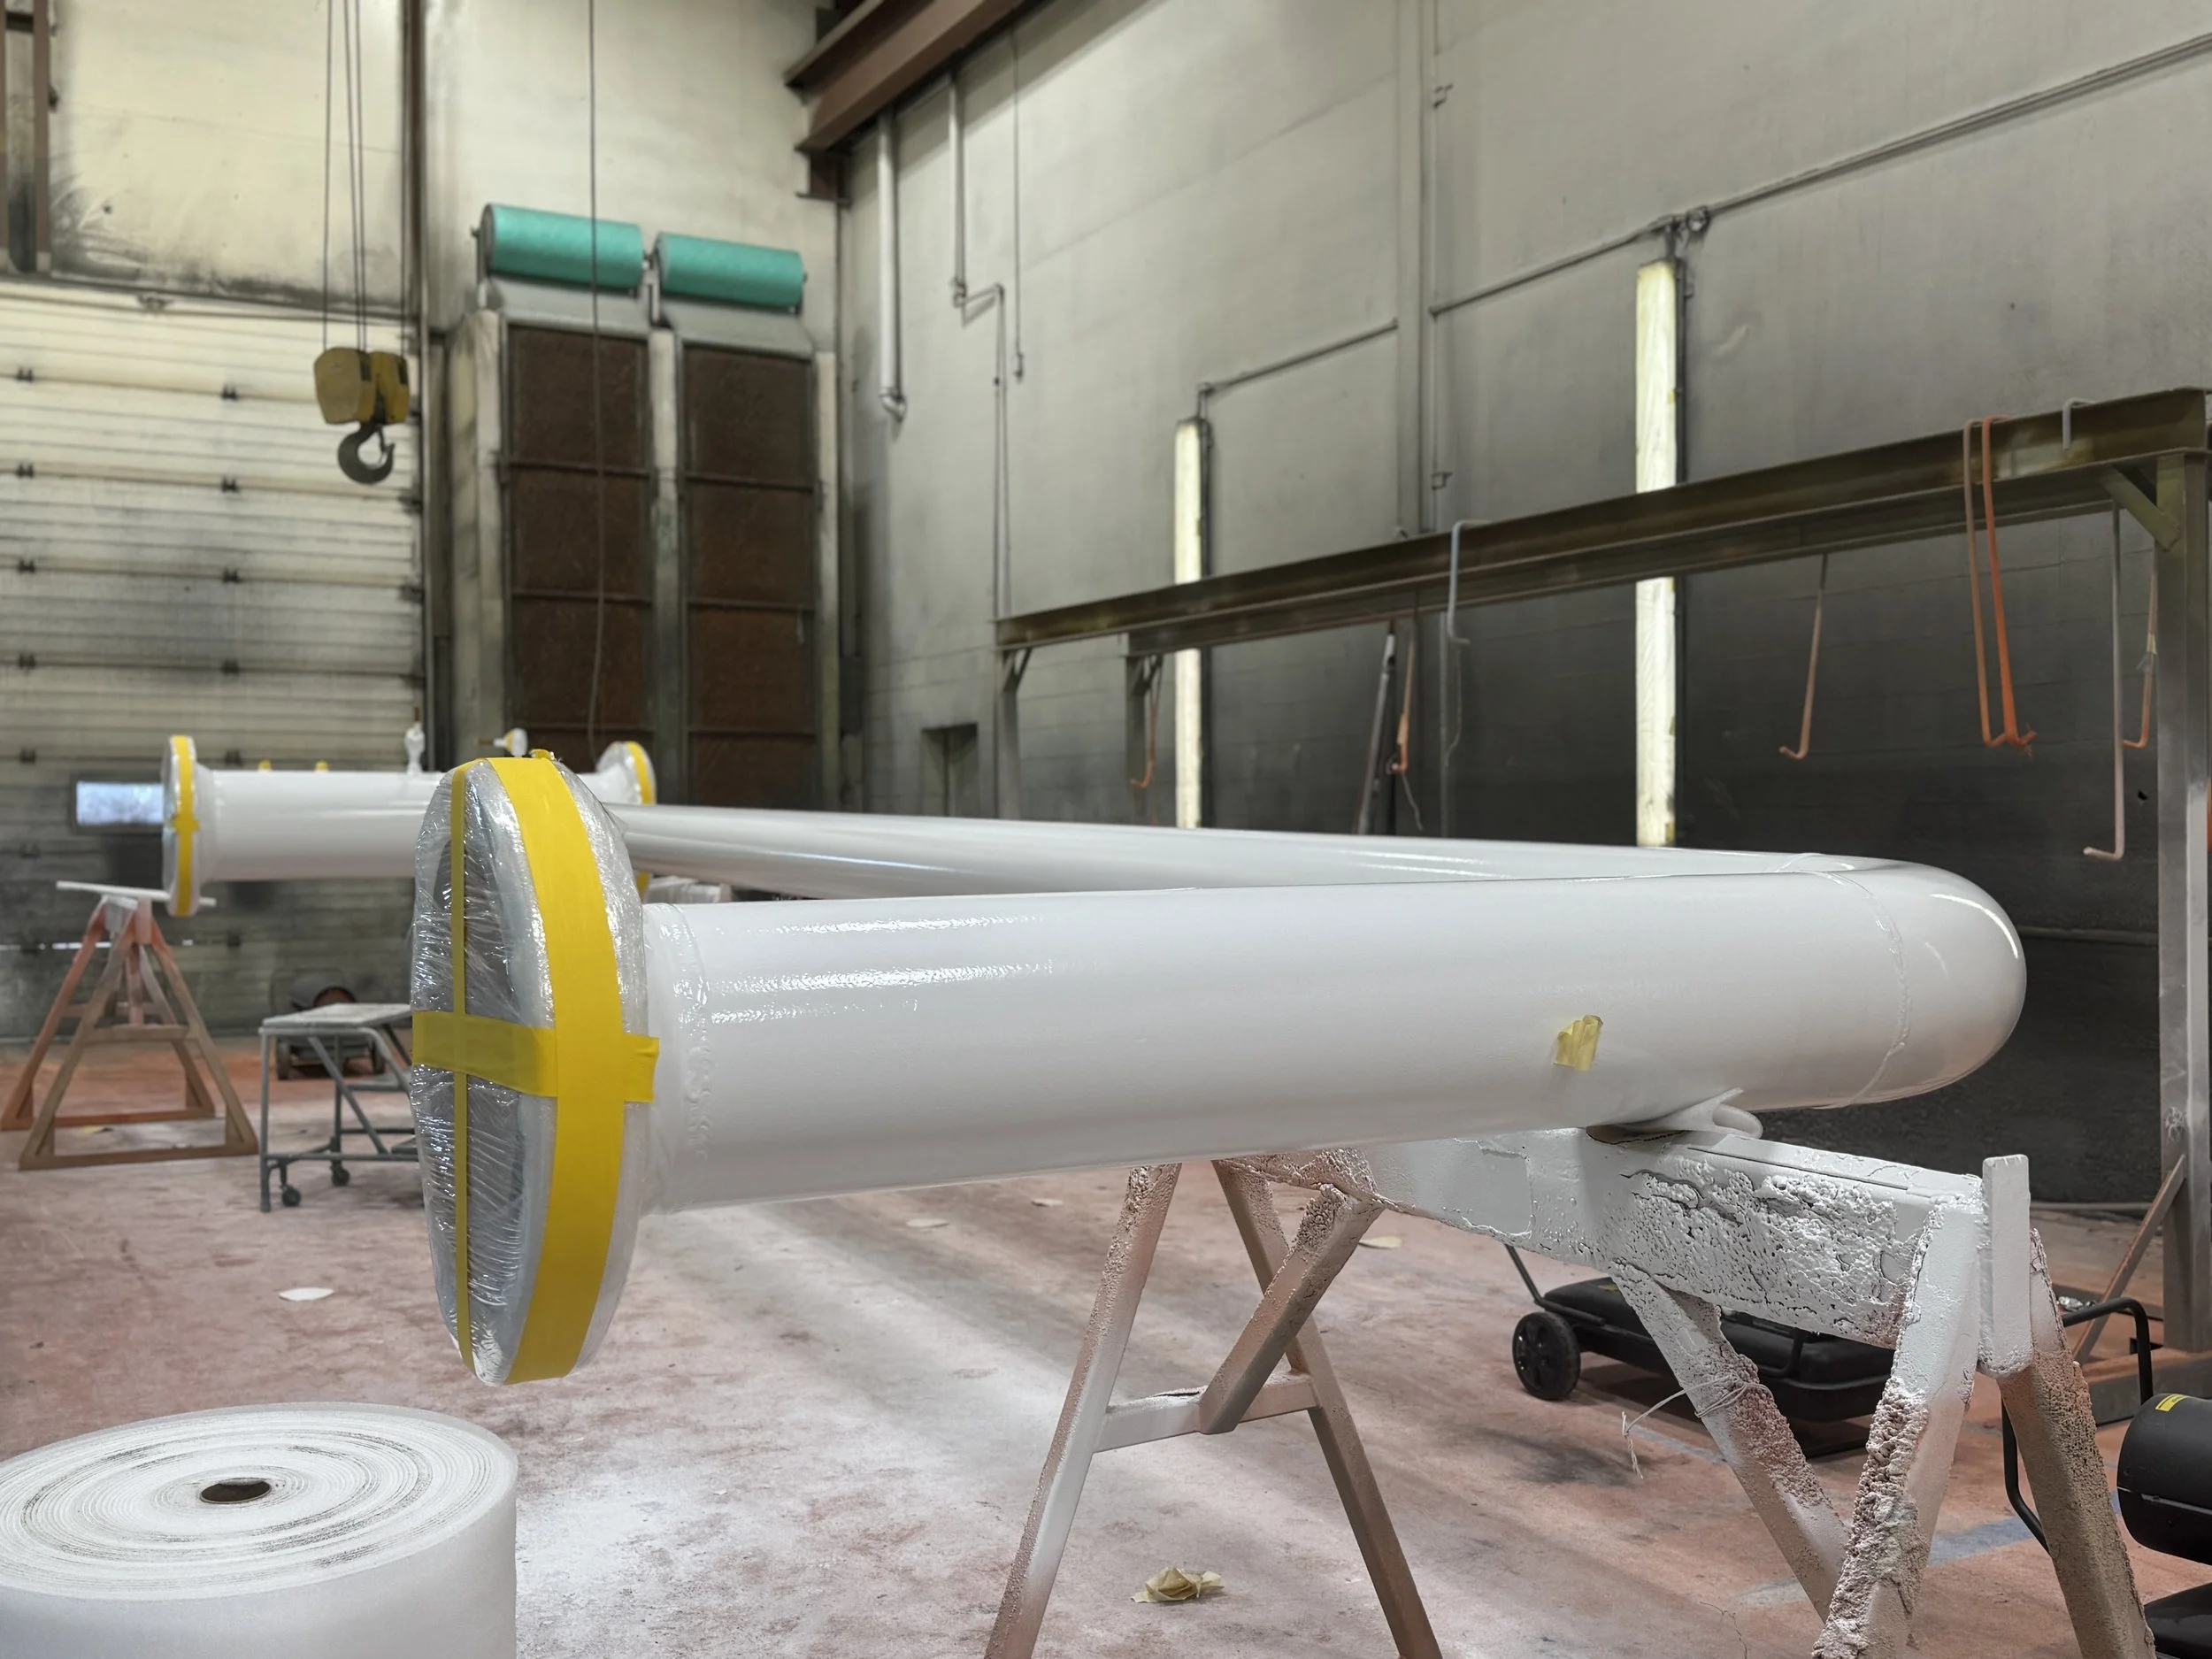
COATING SYSTEMS
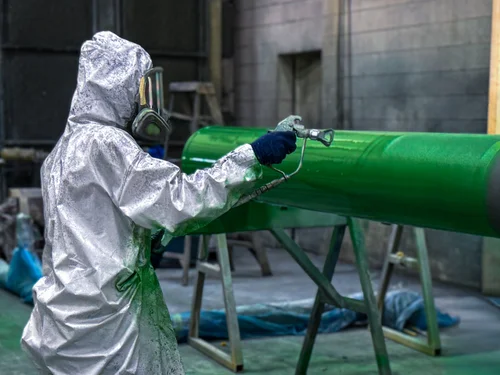
100% Solids Epoxies
Applied with a plural component system, 100% solid coatings are primarily used as a coating application for below-grade pipelines, pipe bends, fittings, valve assemblies, and various below-grade equipment. It is also a suitable system for use on “slip bore” piping where additional abrasion resistance is required.

Liquid-Based Epoxies
Used commonly for internal lining applications in protecting fabricated pipe “spools”. Epoxy coatings act as a barrier to help protect the substrate from corrosion and erosion.
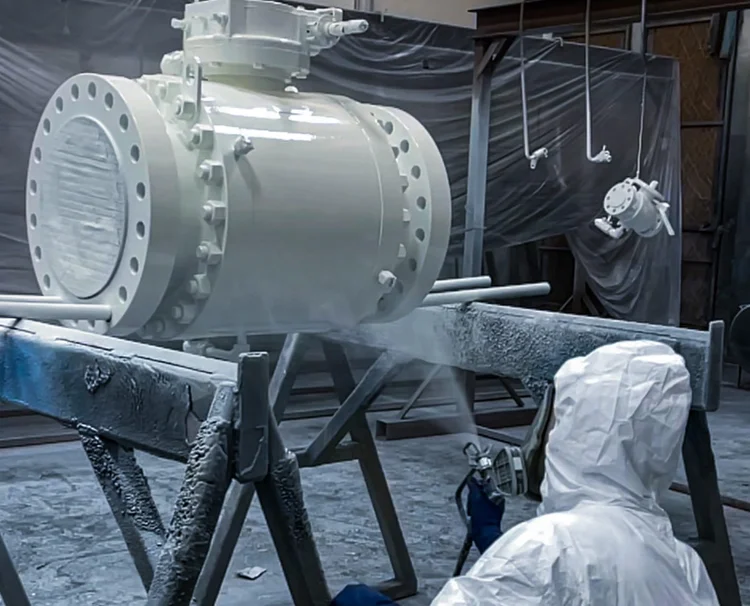
Epoxy & Polyurethane Systems
Considered to be the most durable of all the above-grade coating systems and designed for both functionality and aesthetics. They offer excellent chemical and water resistance. It is common practice to pair an epoxy coating with a UV-resistant coating, such as a polyurethane, to prevent chalking and coating breakdown when in atmospheric service.

Internal Linings
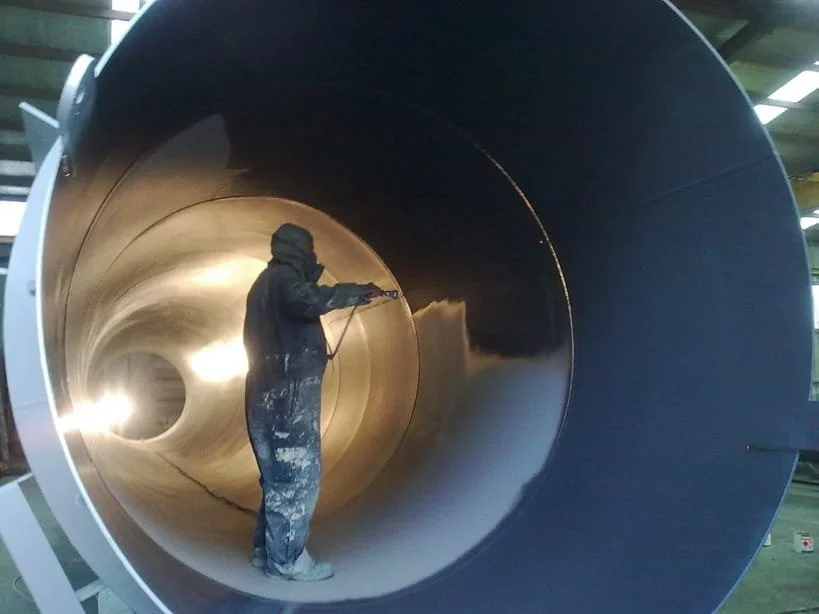
Specialty epoxy coatings commonly used to protect oil treaters, tanks, separators, vessels, or flare knockouts and receiver drums for both immersion and non-immersion. We specialize in coating applications for tanks and vessels that carry acid, downhole chemical “soups”, process water, potable water, and oil.

Alkyd Primer & Paint Systems
Also known as “oil-based” coatings or oleoresins, they have been in use in one form or another for thousands of years. These primers and paints produce a hard and durable film and are a more economical alternative to epoxy / polyurethane systems. Urethane alkyds do offer enhanced chemical resistance and a harder, more abrasion-resistant finish than standard alkyds.

Coatings for Under Insulation
Also known as CUI Coatings, these coatings are generally classified as immersion-grade epoxies and are designed to operate with the cyclical changes in temperatures under insulation on piping and equipment. Temperature cycles can affect humidity levels, creating moisture that may form under the insulation and cause corrosion of the substrate.
BENEFITS OF INDUSTRIAL COATING SERVICES
The advantages of industrial coatings go far beyond aesthetics. While they can improve the appearance of equipment, their primary function is protection. These coatings are designed to resist environmental, chemical, and mechanical stressors that would otherwise cause premature wear and failure. Some of the most important benefits include:
- Corrosion protection → prevents rust and microbiologically induced corrosion, especially in pipelines and marine structures.
- Hardness and durability → thermosetting systems create a tough finish that can withstand heavy loads and daily wear.
- Waterproofing and weatherproofing → protects both indoor and outdoor assets from water intrusion, extreme temperatures, and UV exposure.
- Abrasion and impact resistance → minimizes wear on moving components, extending equipment life.
- Chemical resistance → withstands contact with aggressive industrial solvents, fuels, and process chemicals.
- Thermal protection → certain coatings are engineered to resist heat, fire, and stress cracking.
- Cost-effectiveness → lowers maintenance and replacement expenses, providing long-term savings.
By serving as an engineered shield, industrial coatings paintings help companies maximize uptime, reduce operational risks, and improve the performance of critical infrastructure.
INDUSTRIAL COATINGS INDUSTRY APPLICATIONS
Pipes & piping systems
Downstream pipes, spools, bends, anchors, and tubular joints.
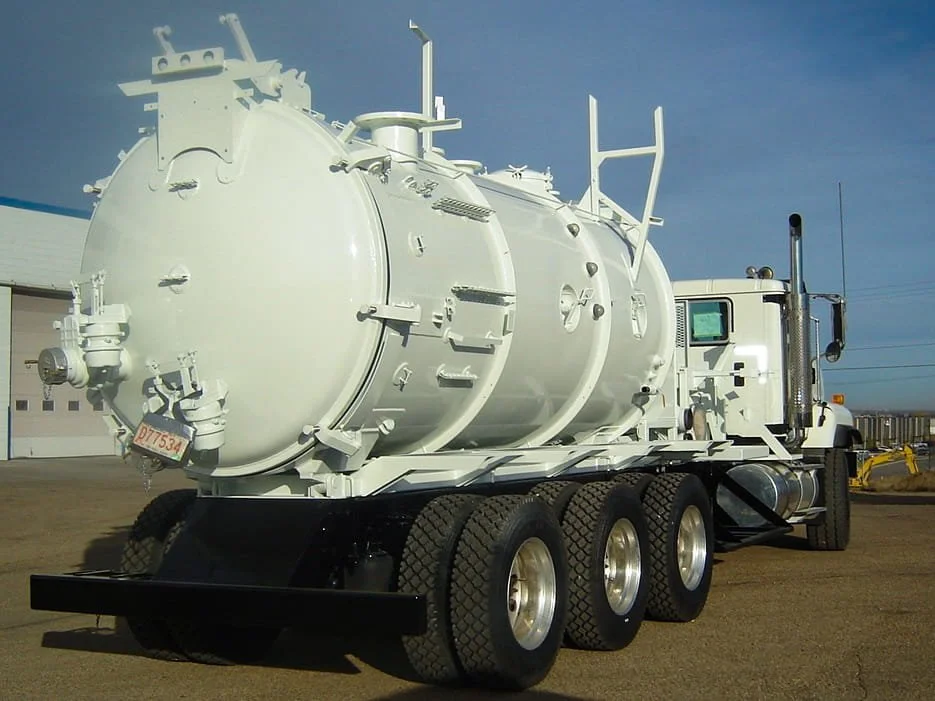
Oilfield & petrochemical equipment
Tanks, skid systems, separators, and pressure vessels.
Construction and infrastructure
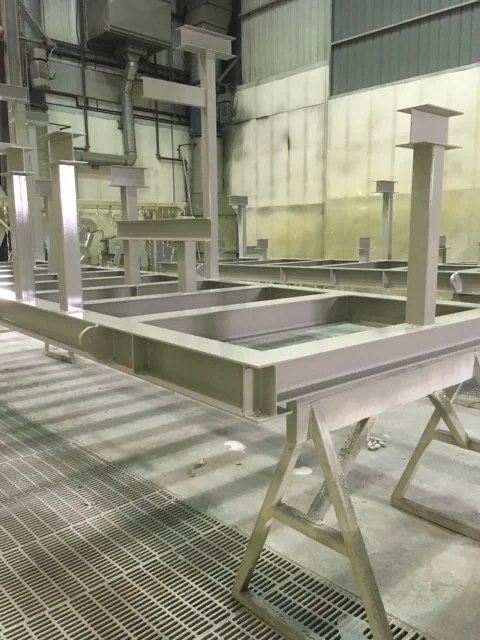
Structural steel, screw piles, handrails, kick plates, and containment tanks.
Marine applications
Ships, offshore platforms, and submerged components.
Automotive & agricultural equipment
Gears, pumps, motors, valves, and fasteners.
Credentials
- ISO 9001-certified, ISN member contractor, and COR-certified
- NACE Level 1 & 2 Certified Coating Inspectors on staff, with NACE Level 3 Certified Coating Inspectors available upon request
Quality Assurance & Control
- Surface preparation to SSPC/NACE standards, with profile measured and recorded per specification
- Climate-controlled blast and coating bays for proper application and cure
- QC testing, including ambient condition monitoring and DFT readings provided in every project
- X-cut adhesion, compressed air (blotter), dust, and soluble salt testing, and holiday testing available upon request
- Inspection and Test Plans (ITPs) and QC documentation available upon request
WHY CHOOSE CUSTOM COATINGS INTERNATIONAL?
CCI has invested significant resources in building and strengthening our quality assurance and control department, training our team to ensure every project meets specifications.
REQUEST A QUOTE
To initiate the quoting process, please provide the following information (if available):
• Drawings or isometrics
• Coating specifications
• Operating environment details (temperature range and chemical exposure)
• Project timeline or required completion date
We look forward to working with you on finding the right protective coating for your project. If you have any questions, please contact us using the links below.

Info@ccintl.ca for general inquiries

sales.support@ccintl.ca for quote requests
INDUSTRIAL COATINGS FAQ
-
Industries such as oil & gas, marine, construction, and automotive benefit the most due to their exposure to corrosion, chemicals, and heavy mechanical stress.
-
No. They can also be applied during refurbishment projects to extend the service life of older equipment and reduce replacement costs.
-
Lifespan depends on the coating type and service environment. With proper application and maintenance, coatings can last many years, even in extreme conditions.
INDUSTRIAL COATINGS GALLERY